
 English
 русский
 Português
 Français


 Read More
Product Category
NEW Category
Contact us
Contact Us
We specialise in the research, development and manufacture of electrical wires and cables.
 +86-21-57560276
Bottom-Entry High-Shear Magnetic Emulsifier for Hygienic Food and Biopharmaceutical Processing
Content
- 1 1. The Processing Challenges Behind High-Shear Emulsification
- 2 2. Product Overview
- 3 3. How the Magnetic Drive Improves Process Containment
- 4 4. Bottom-Mounted Installation and Vessel Utilization
- 5 5. Impeller Geometry and Controlled Shear
- 6 6. Hygienic Materials and Product-Contact Construction
- 7 7. Operating Range and Model Selection
- 8 8. Advantages Over Conventional Mechanical Mixing Equipment
- 9 9. Applications in Biopharmaceutical Manufacturing
- 10 10. Applications in Food and Beverage Production
- 11 11. Manufacturing Capabilities and Engineering Strengths
- 12 12. Engineering Support from Selection to Commissioning
- 13 13. Quality Management and Documentation
- 14 14. Safety and Operating Considerations
- 15 15. Comparison of the LMP, LHS, LHS-G, and LDC Series
- 16 16. Practical Benefits for Total Cost of Ownership
- 17 17. Recommended Project Workflow
- 18 18. Frequently Asked Questions
- 18.1 What is the primary purpose of a bottom-entry high-shear magnetic emulsifier?
- 18.2 How does the magnetic drive reduce contamination risk?
- 18.3 What is the maximum speed of the high-shear model?
- 18.4 Can the equipment process high-viscosity materials?
- 18.5 What materials are used for product-contact components?
- 18.6 Why are tungsten carbide bearings used?
- 18.7 Is the mixer suitable for CIP and SIP systems?
- 18.8 Which series is best for emulsification and particle size reduction?
- 18.9 Can the equipment be used in cell reactors?
- 18.10 What information is needed for equipment selection?
- 18.11 What manufacturing support is available?
- 19 19. Conclusion
- 20 References
- 21 Product: Bottom-entry High-shear Magnetic Emulsifier
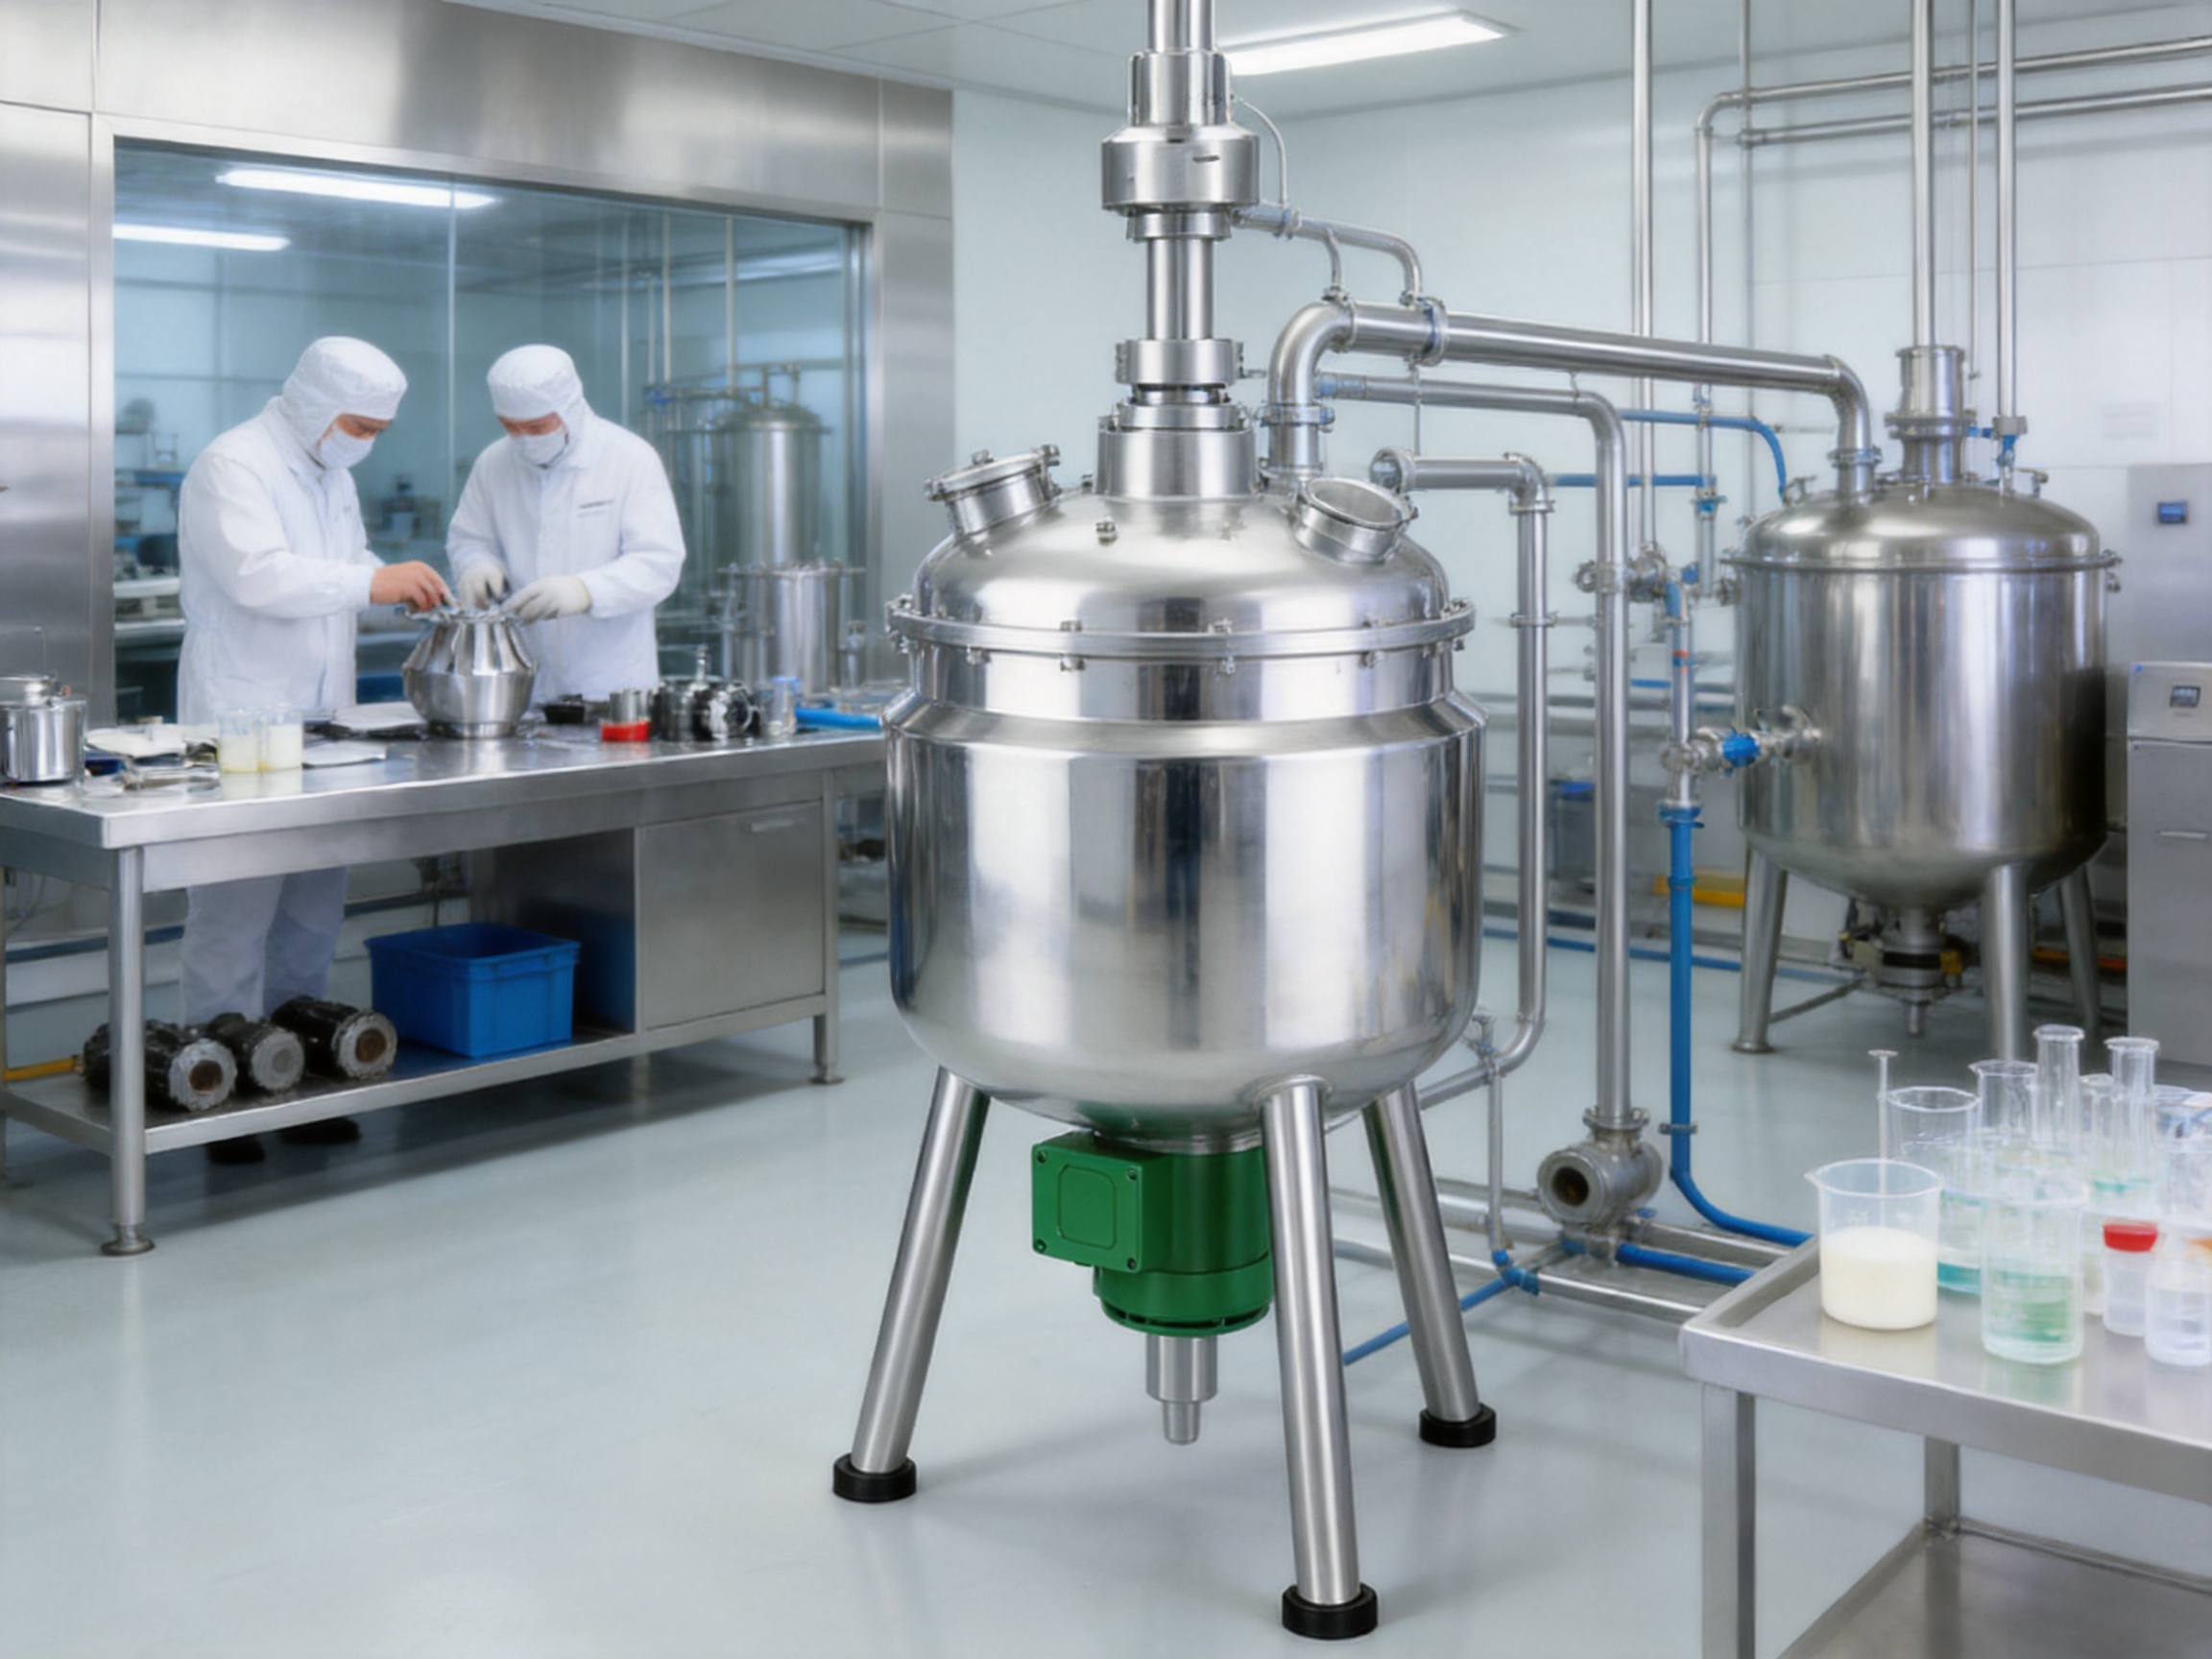
Modern food, beverage, pharmaceutical, and biotechnology manufacturers increasingly require process equipment that can combine high mixing performance with hygienic design, reliable containment, straightforward cleaning, and efficient use of plant space. These requirements become especially important when a process involves difficult-to-wet powders, high-value ingredients, sensitive biological materials, suspensions, emulsions, or products that must be handled in a sterile environment.
The Bottom-entry High-shear Magnetic Emulsifier is designed for these demanding applications. It combines bottom-mounted installation, magnetic drive technology, optimized impeller geometry, tungsten carbide sliding bearings, and stainless-steel product-contact parts. The result is a compact and hygienic mixing solution for particle size reduction, emulsification, dispersion, dissolution, dilution, and suspension maintenance.
Compared with conventional top-entry agitators or mechanically sealed mixers, the equipment provides several practical advantages. Its magnetic drive minimizes the need for traditional dynamic shaft seals, reducing the risk of leakage and external contamination. Its bottom-entry arrangement saves space above the vessel and promotes circulation from the lower section of the tank. Its high-speed impeller produces controlled shear for applications that require finer dispersion or more uniform emulsification.
The equipment is suitable for selected applications with viscosities up to approximately 800 cP. Actual performance depends on vessel geometry, formulation characteristics, solids concentration, temperature, viscosity, gas content, and the required particle size distribution. Proper model selection should therefore be based on process testing and the properties of the actual medium rather than on water-based capacity figures alone.
1. The Processing Challenges Behind High-Shear Emulsification
Many manufacturing processes appear to require only simple agitation, but the actual mixing task may be significantly more complex. A powder may float on the liquid surface instead of becoming wetted. A dense solid may settle rapidly after mixing stops. Two immiscible liquids may separate soon after entering the vessel. A biological formulation may require uniform distribution without excessive heat generation or uncontrolled mechanical stress.
Traditional mixing equipment can sometimes produce acceptable results, but performance may become inconsistent as formulation viscosity, solids loading, or production scale increases. A basic propeller may circulate liquid without providing enough local shear. A conventional turbine may create strong turbulence but may not efficiently draw floating powder into the liquid. A mechanically sealed agitator may provide adequate mixing but introduce maintenance requirements and potential leakage points.
High-shear magnetic emulsification addresses these challenges by combining circulation and localized mechanical energy. The impeller creates a controlled flow field within the vessel while generating higher shear zones near the impeller. These zones help break down agglomerates, increase contact between solids and liquids, and improve the distribution of droplets or particles throughout the working volume.
Particle size reduction is not achieved by speed alone. The shape of the impeller, the clearance from the vessel bottom, the direction of flow, the residence time within the high-shear zone, and the physical properties of the product all influence the final result. A properly engineered high-shear mixer can therefore deliver more consistent performance than equipment selected only according to nominal motor power or maximum rotational speed.
2. Product Overview
The Bottom-entry High-shear Magnetic Emulsifier is a vessel-mounted mixing system intended for hygienic process applications. It is installed through the lower section of the tank, allowing the mixing element to operate close to the vessel bottom. This arrangement can improve the movement of settled materials and reduce stagnant areas that may occur in poorly designed mixing systems.
The drive system uses magnetic coupling between an external rotor and an internal rotor. The motor turns the external rotor, and magnetic force transfers the rotation through the containment structure to the internal rotor and impeller. Because the rotating shaft does not require a conventional dynamic seal passing through the vessel boundary, the design helps limit product leakage and reduces the possibility of contamination from the surrounding environment.
The product is designed for applications in the pharmaceutical and biotechnology industries and is also suitable for food, beverage, daily chemical, and fine chemical production. Product-contact components are manufactured from 1.4435 or 1.4404 stainless steel, materials commonly selected for hygienic process equipment because of their corrosion resistance, cleanability, and suitability for controlled manufacturing environments.
Sliding bearings are made of tungsten carbide. This material provides high hardness and wear resistance, which is important when the mixer operates at elevated speed or when the processed medium contains suspended particles. The final selection of bearing materials and operating conditions must be evaluated against the formulation and cleaning chemistry used at the installation site.
The high-shear configuration reaches a maximum speed of approximately 2,850 rpm in the LHS-G series. Other magnetic mixer configurations are available for lower-shear duties, including suspension maintenance, dissolution, and general solid-liquid mixing. This product family allows a process engineer to select the appropriate mixing intensity without applying an unnecessarily aggressive shear profile to every formulation.
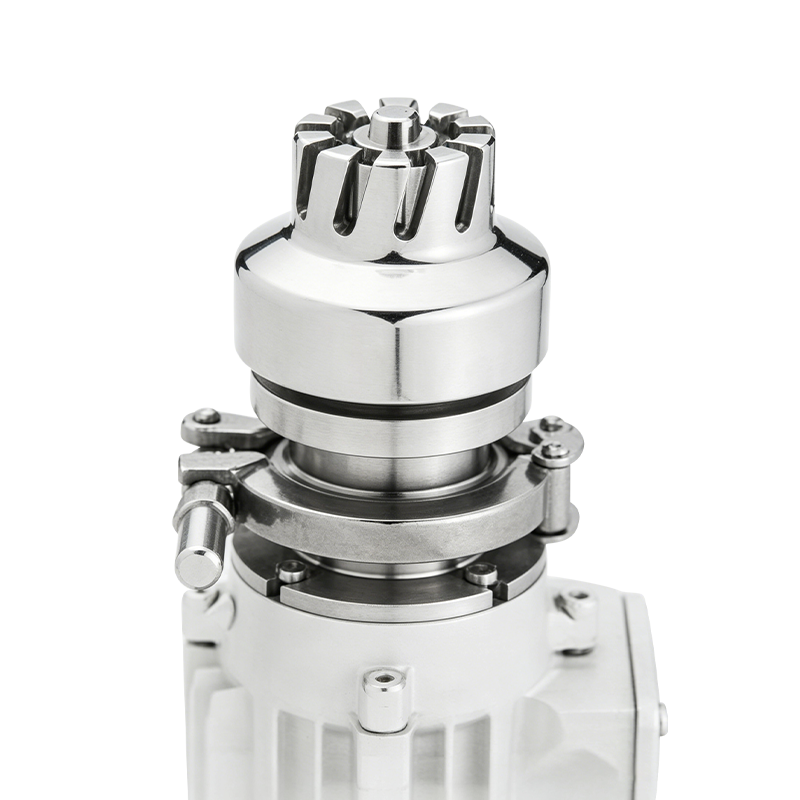
Bottom-entry High-shear Magnetic Emulsifier
3. How the Magnetic Drive Improves Process Containment
Containment is one of the most important design considerations in pharmaceutical, biotechnology, and high-value food production. A mechanical agitator usually requires a rotating shaft to pass through the tank wall. The shaft penetration must be protected by a mechanical seal or another dynamic sealing arrangement. Although modern mechanical seals can perform reliably, they remain components that require correct installation, lubrication or flushing where applicable, inspection, and eventual replacement.
The magnetic drive structure provides an alternative approach. The motor rotates an external magnetic assembly, while an internal magnetic assembly rotates the impeller on the product side. A static containment boundary separates the product from the motor and the external environment. This arrangement reduces the number of moving penetration points and helps prevent the processed medium from escaping through a conventional shaft seal.
This benefit is particularly valuable when the product is toxic, sterile, expensive, oxygen-sensitive, or otherwise vulnerable to environmental exposure. If a seal failure occurs in a conventional system, product leakage may create a safety issue, a contamination risk, or a costly product loss. A properly designed magnetic drive can reduce these risks and simplify the containment strategy.
Magnetic coupling also supports cleaner equipment operation. Because the drive assembly is separated from the process fluid, the motor and gearbox can be maintained without direct contact with the product. This separation is useful in plants where equipment cleaning, changeover, and contamination control are essential parts of the operating procedure.
The magnetic drive should not be regarded as a substitute for complete process validation. The vessel, containment structure, gaskets, welds, bearings, cleaning cycle, sterilization cycle, and operating parameters must all be evaluated as a complete system. However, the seal-free or reduced-seal concept provides a strong foundation for hygienic equipment design and can offer an advantage over traditional mechanically sealed agitators.
4. Bottom-Mounted Installation and Vessel Utilization
Top-entry agitators require a dedicated area above the vessel for the motor, gearbox, shaft, mechanical seal, and maintenance access. In facilities with restricted headroom, this arrangement can complicate plant layout. It may also interfere with powder charging systems, spray devices, inspection ports, filtration equipment, or other top-mounted components.
A bottom-mounted mixer moves the main drive arrangement away from the top of the vessel. This can save operational space and give process designers more flexibility when configuring the tank. The upper section of the vessel can remain available for charging, sampling, spray balls, sensors, filters, or other process connections.
The bottom-entry position also places the impeller near the lowest part of the vessel. This is useful for applications where solids settle quickly or where the process requires effective movement of material from the bottom region into the main circulation loop. When the impeller and vessel geometry are correctly matched, the mixer can help reduce dead zones and improve overall tank turnover.
Bottom mounting is not automatically ideal for every application. The vessel must be designed to support the equipment, and the bottom nozzle, flange, welds, internal clearance, and drainability must be properly engineered. The product should also be positioned to avoid interference with heating surfaces, internal coils, load cells, or other vessel components.
For installations requiring frequent cleaning or sterilization, the bottom connection must be designed with appropriate hygienic features. Smooth surfaces, controlled crevices, suitable gasket arrangements, and proper drainage are important for achieving consistent CIP and SIP performance.
5. Impeller Geometry and Controlled Shear
The impeller is the primary process-working element of the emulsifier. Its geometry determines how the product moves through the vessel and how much energy is introduced into the liquid. The design goal is not simply to create the highest possible turbulence. Instead, the impeller must create an effective combination of bulk circulation, localized shear, particle wetting, and energy transfer.
The impeller used in a high-shear magnetic emulsifier creates a focused mixing flow field. At the same time, its profile produces moderate to high shear rates suitable for demanding applications. This balance allows the equipment to process powders, liquids, and suspended materials while reducing the risk of unnecessarily damaging sensitive formulations.
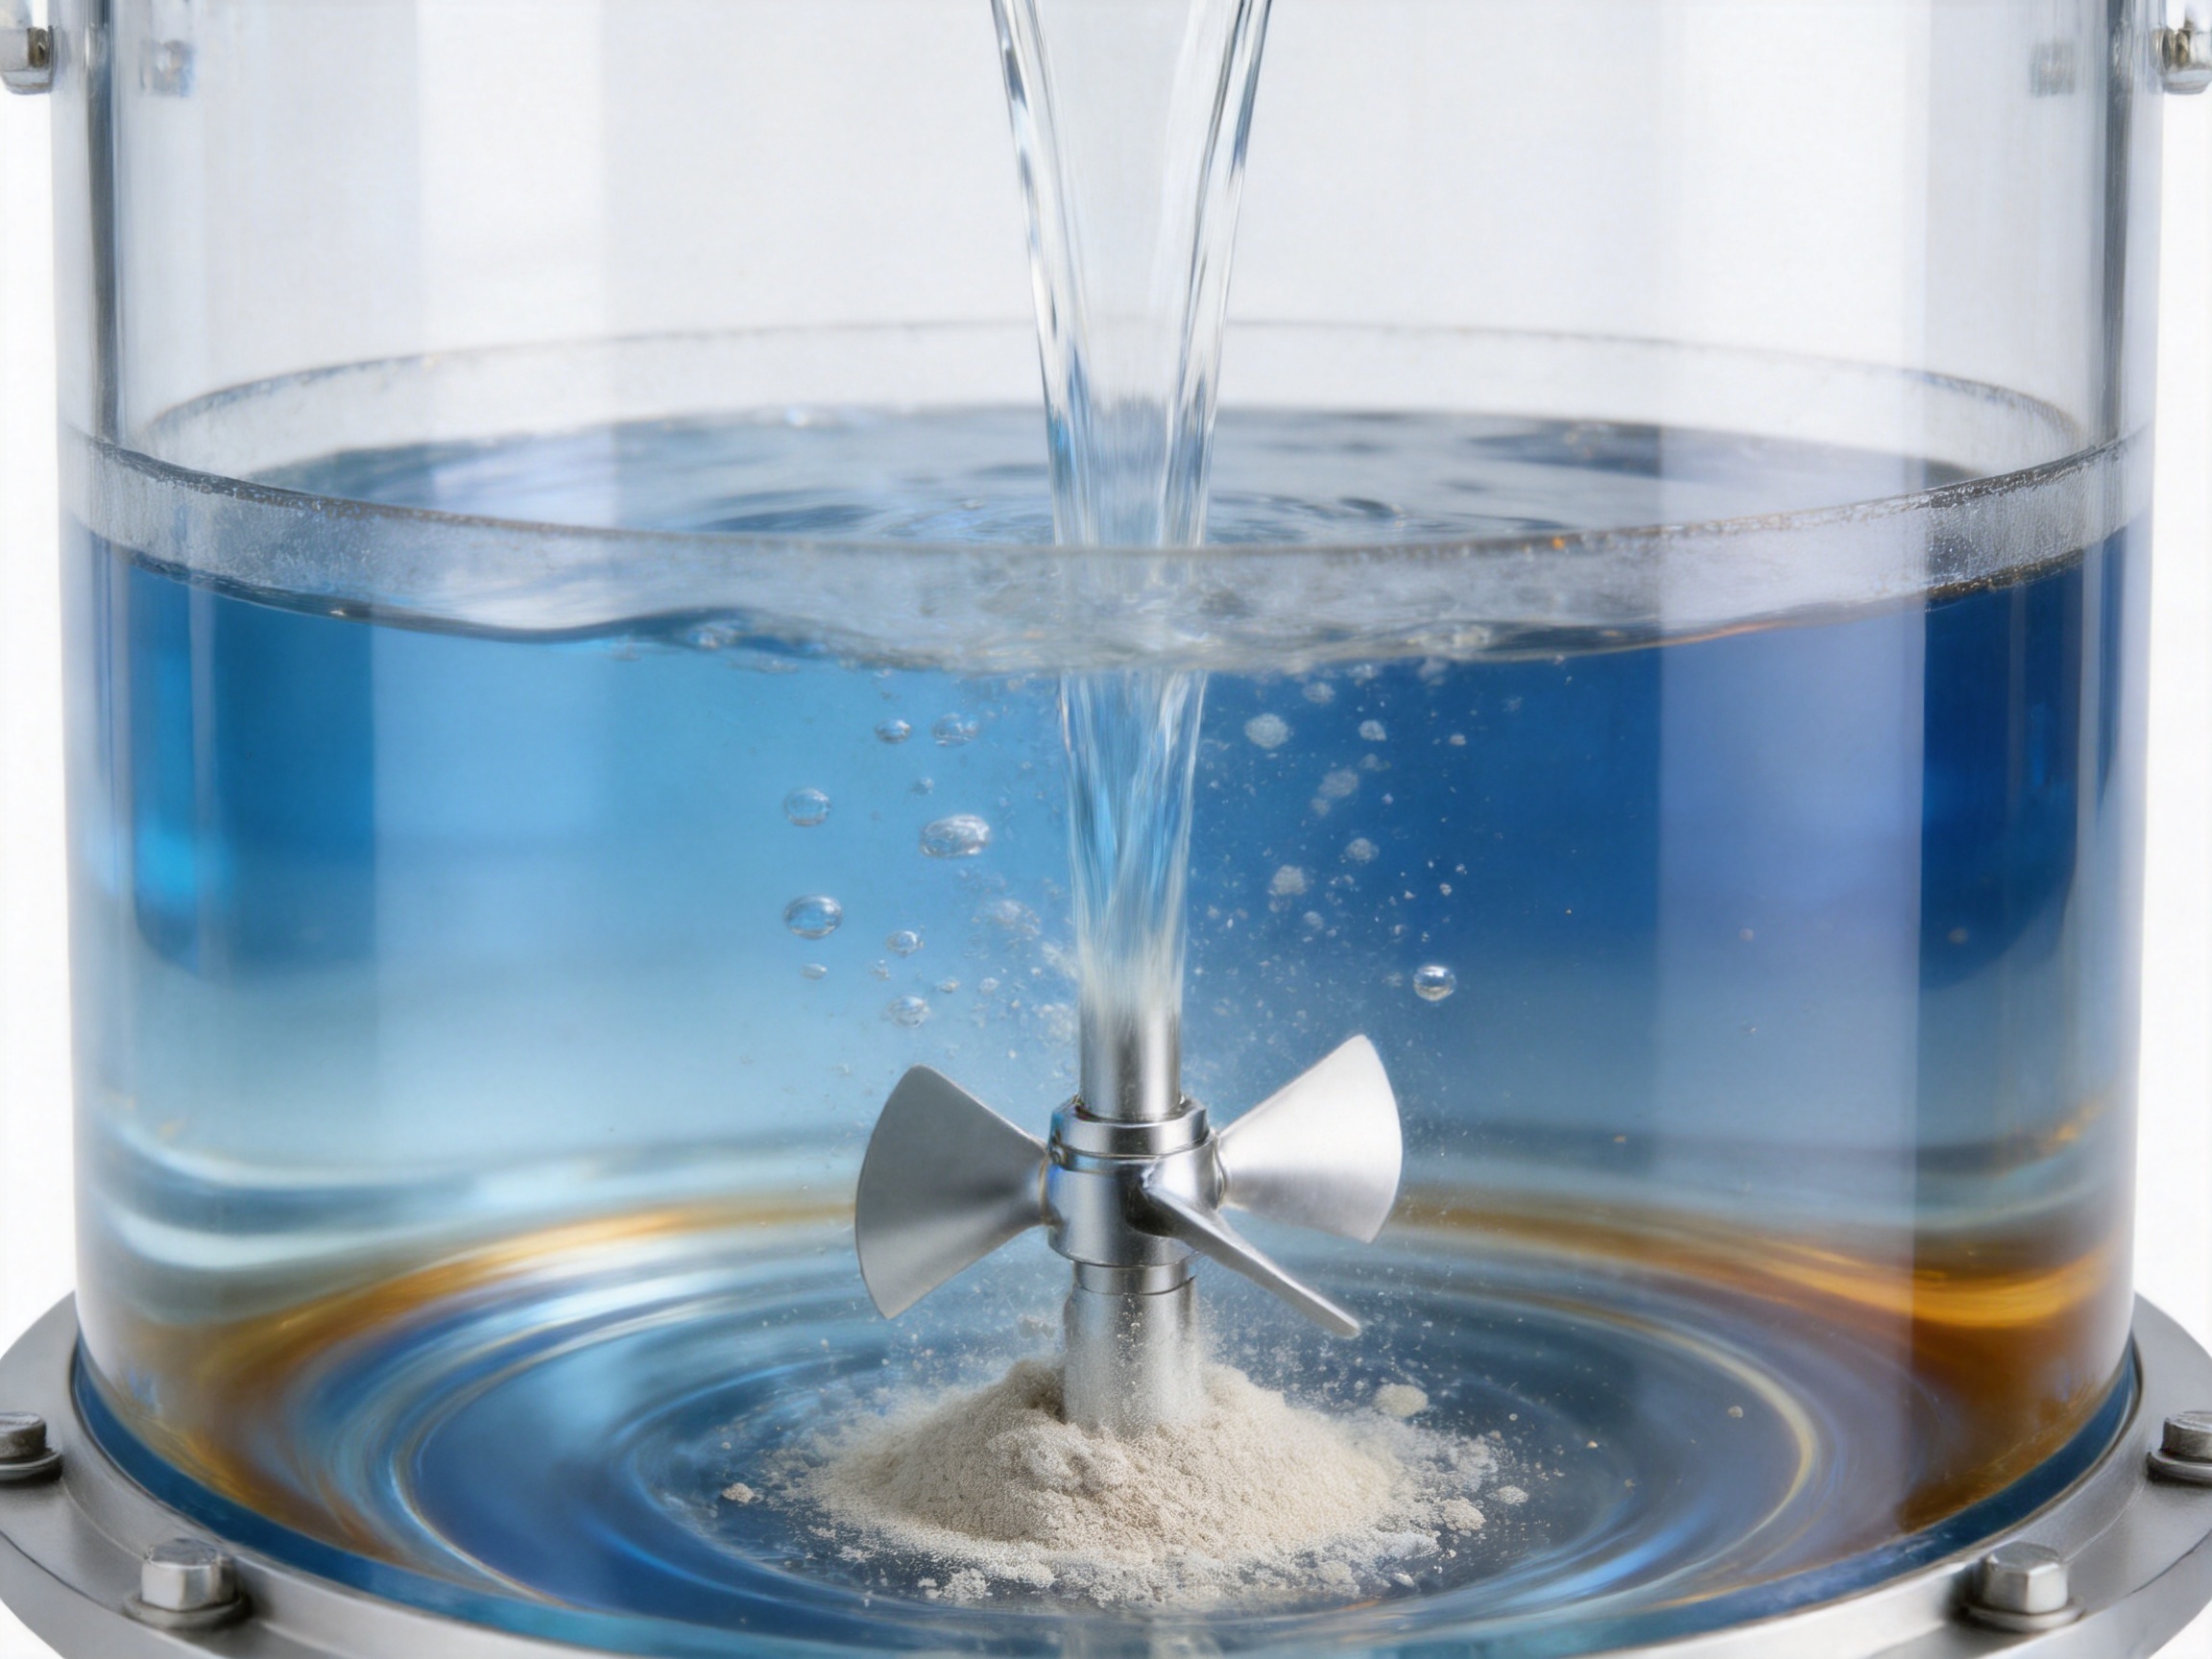
When powder is added to a liquid, the first challenge is often wetting. Dry particles can form floating layers or agglomerates that resist penetration. The impeller must draw the material into the liquid and expose fresh particle surfaces to the surrounding phase. Once the powder is wetted, the shear field can break apart agglomerates and improve the uniformity of the dispersion.
During emulsification, the impeller helps divide one liquid phase into smaller droplets within another phase. Droplet size depends on shear intensity, interfacial tension, formulation chemistry, temperature, residence time, and the ratio of the two liquid phases. A high-shear mixer can promote smaller and more uniform droplets, but the final result still depends on the formulation and the complete process sequence.
In suspension applications, the impeller maintains movement throughout the vessel and helps prevent solids from settling. In dissolution processes, it improves contact between the solid material and the liquid phase. In dilution, it helps distribute a concentrated addition more rapidly and consistently.
6. Hygienic Materials and Product-Contact Construction
All product-contact surfaces are manufactured from 1.4435 or 1.4404 stainless steel. These grades are selected for their suitability in hygienic and corrosion-resistant equipment. The exact material choice may depend on the process chemistry, chloride exposure, cleaning agents, temperature, and customer specifications.
Material selection is only one part of hygienic design. Surface finish, weld quality, geometry, drainage, gasket selection, and inspection procedures are equally important. Product-contact areas should be designed to minimize crevices and inaccessible pockets where residues could collect. Welds should be properly prepared and finished to support cleaning and reduce the risk of corrosion initiation.
The equipment is designed to support CIP and SIP requirements. Clean-in-place systems use controlled flows of cleaning solutions to remove product residues without disassembling the mixer. Steam-in-place systems expose the equipment to validated steam cycles for sterilization. The actual cleaning and sterilization results depend on the installation, flow velocity, chemical concentration, temperature, time, and validation procedure.
A sterile design is especially important in biopharmaceutical applications. In these environments, a small contamination event may affect an entire batch or disrupt a carefully controlled biological process. The magnetic drive, hygienic contact materials, and cleanable configuration are intended to support a closed and controlled production system.
The equipment can also be used in food and beverage processing, where cleanability, product changeover, and avoidance of cross-contact are critical. Applications may include beverage concentrates, nutritional products, sauces, dressings, dairy-related formulations, flavor systems, and other liquid or semi-liquid products. Each application requires an evaluation of viscosity, solids, temperature, shear sensitivity, and cleaning chemistry.
7. Operating Range and Model Selection
The product family includes several magnetic mixer configurations. The LHS-G series is the high-shear option and reaches a maximum speed of approximately 2,850 rpm. The LHS series low-shear model reaches approximately 1,480 rpm. LMP models operate at lower speeds and are intended for suspension, dissolution, dispersion, and other general mixing tasks.
| Product type | Maximum speed | Typical application focus |
|---|---|---|
| LDC-N top-mounted magnetic mixer | 600 rpm | Solid-liquid mixing, dispersion, dissolution, and CIP/SIP-compatible processing |
| LDC-W top-mounted magnetic mixer | 1,200 rpm | Dispersion, suspension, solution preparation, and higher-speed top-entry mixing |
| LMP-S bottom-mounted magnetic mixer | 500 rpm | General mixing, suspension, dissolution, and dispersion |
| LMP-D bottom-mounted magnetic mixer | 480 rpm | Multi-zone circulation and cell reactor applications |
| LHS bottom-mounted magnetic mixer | 1,480 rpm | Low-to-moderate shear dispersion, mixing, suspension, and dissolution |
| LHS-G bottom-mounted high-shear mixer | 2,850 rpm | High-shear emulsification, fine dispersion, and particle size reduction |
Model selection should begin with the process objective. If the main requirement is to maintain a uniform suspension with limited shear, an LMP or LHS configuration may be more appropriate than an LHS-G model. If the process requires emulsification, agglomerate breakdown, rapid powder incorporation, or particle size reduction, the high-shear LHS-G model may provide a more suitable operating profile.
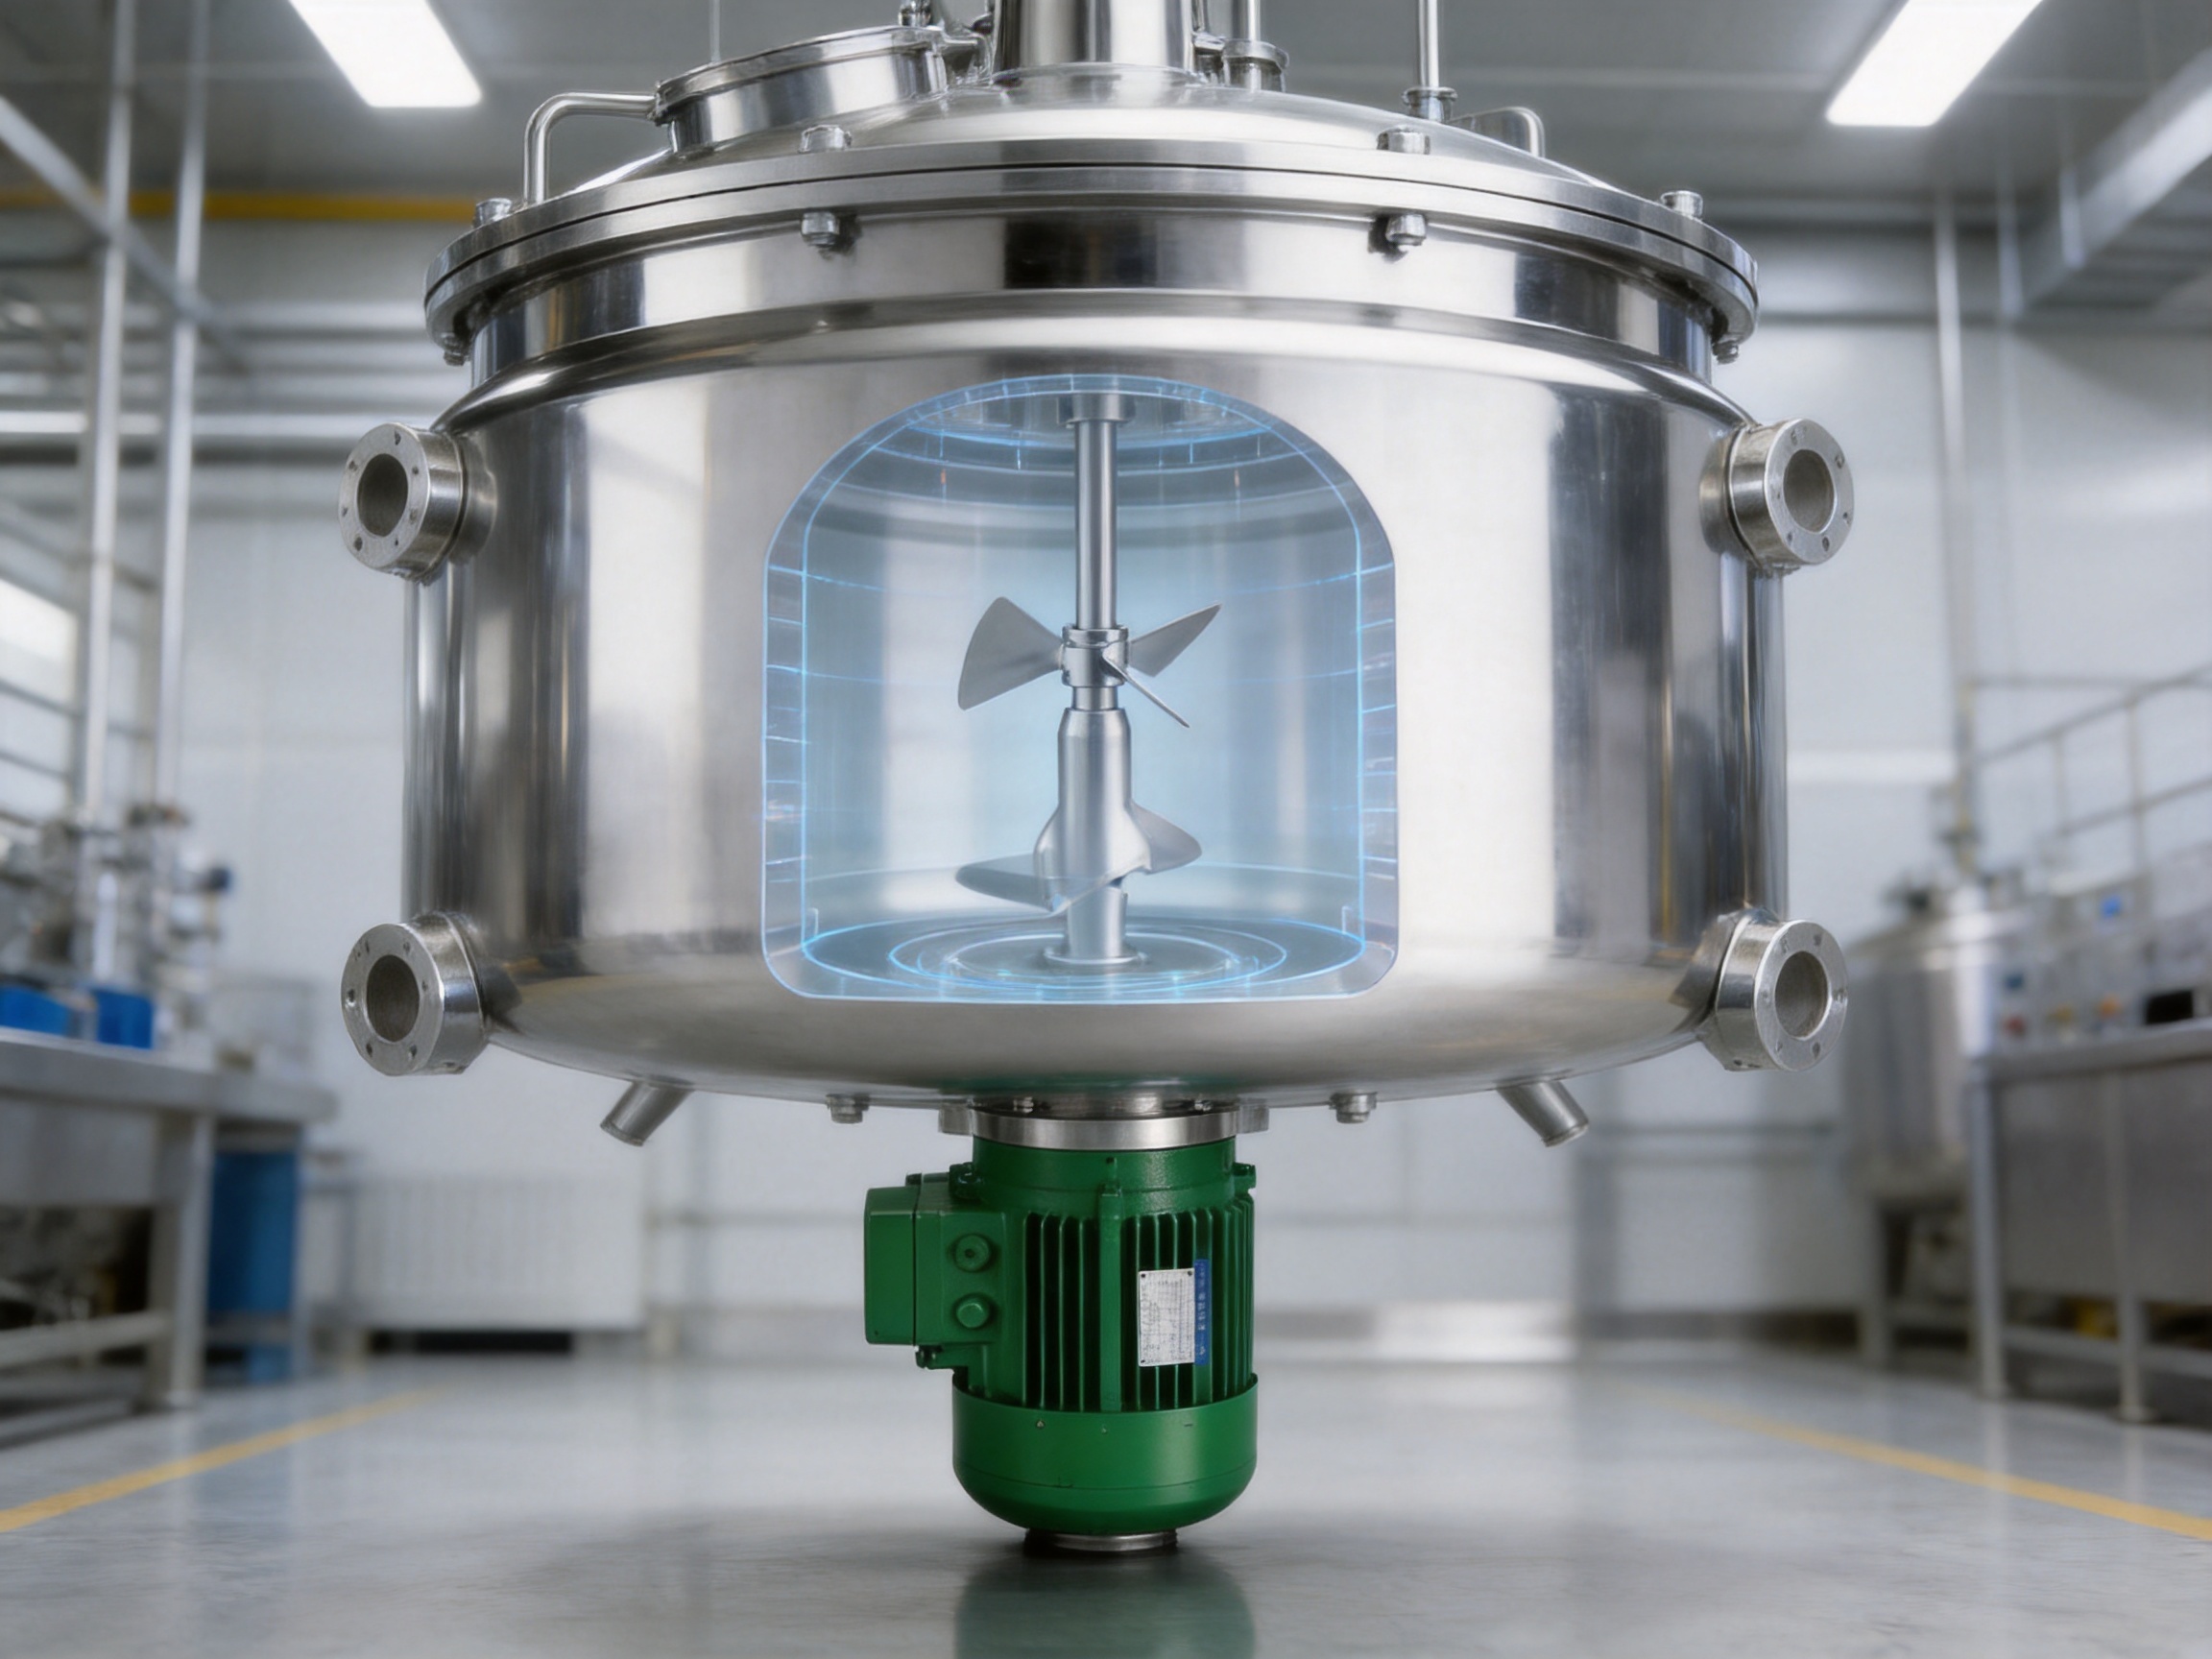
Vessel volume is another important factor. The LHS-G150 is designed for approximately 10 to 150 liters under water-based testing conditions. The LHS-G600 is intended for approximately 150 to 600 liters, while the LHS-G2500 is intended for approximately 600 to 2,500 liters. These values are reference capacities and should not be treated as universal guarantees for every product.
| Model | Blade diameter | Power range | Speed | Reference capacity |
|---|---|---|---|---|
| LHS-G150 | 80 mm | 0.55/0.75 kW | 2,850 rpm | 10–150 liters |
| LHS-G600 | 100 mm | 2.2/3 kW | 2,850 rpm | 150–600 liters |
| LHS-G2500 | 170 mm | 5.5/7.5 kW | 2,850 rpm | 600–2,500 liters |
Water-based capacity testing provides a useful reference, but actual operating capacity can change significantly when the medium has higher viscosity, elevated solids loading, non-Newtonian behavior, or strong temperature dependence. The correct selection should therefore consider rheology, batch size, desired processing time, torque, power density, heat generation, and required final quality.
8. Advantages Over Conventional Mechanical Mixing Equipment
The first major advantage is reduced contamination and leakage risk. Conventional shaft seals can be reliable, but they remain a possible source of product leakage or environmental ingress. The magnetic drive removes the need for a conventional rotating shaft penetration through the product boundary, supporting a more contained process arrangement.
The second advantage is reduced exposure of valuable or hazardous media. In pharmaceutical, biotechnology, and specialty chemical production, even a small leak can cause significant financial, safety, or regulatory consequences. The magnetic drive helps protect the product and the surrounding workplace by maintaining separation between the process side and the drive side.
The third advantage is the bottom-entry configuration. Compared with many top-entry designs, the equipment uses less space above the tank. This can reduce layout constraints and make it easier to integrate powder charging, sensors, filters, and cleaning devices in the upper vessel area.
The fourth advantage is high-shear performance in a hygienic format. Some high-shear mixers use arrangements that are difficult to clean or unsuitable for sterile production. This product combines high-speed mixing with CIP/SIP-oriented design principles and product-contact materials selected for hygienic processing.
The fifth advantage is flexibility across process duties. The broader magnetic mixer range includes high-shear, low-shear, top-mounted, single-layer, and multi-layer configurations. This allows users to select an appropriate machine rather than forcing one mixer design to perform every type of operation.
The sixth advantage is low start-up volume. A mixer that can operate effectively at a relatively low working volume can help reduce material loss during start-up, testing, and product changeover. This feature may be especially valuable when the processed formulation is expensive or when batch sizes vary substantially.
The equipment also offers a practical maintenance advantage. The drive-side components remain separated from the product, and the absence of a traditional dynamic seal can reduce certain inspection and replacement requirements. Maintenance intervals still depend on speed, load, bearing conditions, cleaning cycles, and operating practice, but the overall arrangement can simplify equipment management.
9. Applications in Biopharmaceutical Manufacturing
Biopharmaceutical production often combines strict contamination control with sensitive product characteristics. The process may involve cell culture media, buffer preparation, active pharmaceutical ingredients, excipients, suspensions, emulsions, or intermediate solutions. Each material may respond differently to shear, temperature, aeration, and residence time.
The high-shear magnetic emulsifier can support preparation steps where powders must be incorporated into liquids, where an emulsion must be stabilized, or where suspended components must remain evenly distributed. Its sealed magnetic drive is appropriate for applications in which the process boundary should remain closed and the possibility of product leakage must be minimized.
For cell-related applications, the process engineer must distinguish between the high-shear LHS-G model and lower-shear alternatives. Some cell systems are sensitive to excessive shear and may require a gentler circulation pattern. The LMP-D multi-layer mixer is identified for cell reactor applications, while the LHS-G model is intended for high-shear emulsification and particle reduction. The appropriate choice depends on the biological material and the desired process result.
In buffer and solution preparation, the equipment can assist with dissolution, dilution, and suspension maintenance. Powdered ingredients that tend to form lumps may be incorporated more efficiently when the impeller creates strong local circulation near the addition zone. A validated addition sequence and suitable feed rate remain essential for achieving repeatable results.
In sterile processing, the equipment should be integrated with a validated cleaning and sterilization strategy. This may include defined CIP flow paths, steam exposure, temperature mapping, pressure control, sterile connections, and documented acceptance criteria. The mixer is one component within a larger hygienic process system, and final compliance depends on the complete installation.
10. Applications in Food and Beverage Production
Food and beverage manufacturers often process products with widely varying viscosities and ingredient profiles. A single plant may handle low-viscosity beverages, concentrated syrups, nutritional products, sauces, dressings, flavor preparations, or suspension-based formulations.
The bottom-entry high-shear configuration can help reduce powder agglomerates and improve the dispersion of ingredients that are difficult to wet. It may also support the preparation of emulsified products where a uniform distribution of oil and water phases is required. The actual droplet size and stability depend on formulation composition, emulsifier selection, temperature, processing time, and the downstream filling or storage conditions.
Hygienic design is particularly important when a facility produces multiple products in the same vessel. Efficient CIP performance can reduce changeover time and help limit cross-contact between batches. The use of corrosion-resistant stainless steel, cleanable geometry, and magnetic containment supports the plant’s overall sanitation strategy.
Bottom mounting may also help food manufacturers optimize compact production rooms. By reducing the equipment installed above the tank, the layout can provide more accessible space for ingredient handling, operator movement, inspection, and cleaning connections.
Food applications may require additional consideration of allergen control, thermal processing, foam formation, solids handling, and product sensitivity. Before final selection, the user should confirm that the impeller speed, power, and shear level are appropriate for the specific recipe.
11. Manufacturing Capabilities and Engineering Strengths
Shiloc (Shanghai) Industrial Trading Co., Ltd. provides equipment manufacturing, engineering and technical services, import and export support, and process equipment solutions for food, beverage, pharmaceutical, biotechnology, daily chemical, and fine chemical industries. The company was established in Shanghai and operates a production facility of approximately 3,000 square meters.
The company’s manufacturing capability includes internal processing, welding, polishing, assembly support, and quality control. These activities are important for hygienic equipment because the quality of the final mixer depends on more than the purchased motor or magnetic coupling. Product-contact surfaces, welded joints, dimensional accuracy, bearing installation, and traceability all affect performance and cleanability.
Internal processing provides greater control over manufacturing sequence and inspection. When machining, welding, polishing, and assembly activities are coordinated within the company’s own production system, engineering teams can respond more efficiently to dimensional changes, customer requirements, and process-specific modifications.
Welding quality is especially significant for stainless-steel hygienic equipment. Welds must maintain structural strength while also supporting cleanability and corrosion resistance. Proper preparation, controlled welding practice, post-weld finishing, and inspection help reduce the possibility of crevices, rough areas, discoloration, or other surface defects.
Polishing is another important process. A suitable surface finish can make it easier to remove product residues during cleaning and can reduce areas where microorganisms or particles may accumulate. The required finish should be established according to the customer’s specification and the application’s hygienic requirements.
Traceability supports consistent manufacturing and service. Material records, production documentation, inspection data, welding information, and component identification can help customers maintain better control over their equipment history. Traceability is particularly valuable in regulated industries, where equipment documentation may be reviewed during qualification, validation, or quality audits.
The company’s technical team includes more than 20 specialists. This supports a project approach in which equipment selection, process analysis, manufacturing, documentation, installation coordination, and after-sales service can be connected rather than treated as isolated activities.
European technical experience and Danish design concepts are incorporated into the company’s equipment development approach. The goal is to combine practical hygienic design, reliable manufacturing, process optimization, and customer-specific engineering. This approach can provide an advantage over suppliers that offer only standard catalog equipment without sufficient application support.
12. Engineering Support from Selection to Commissioning
Successful mixing depends on the relationship between the equipment and the process. A technically advanced mixer may still perform poorly if it is installed in an unsuitable vessel or operated outside its design range. For this reason, engineering support should begin before the model is selected.
The first step is process definition. Important information includes vessel working volume, minimum and maximum batch volume, liquid density, viscosity range, solids concentration, particle size, temperature, gas content, desired mixing time, shear sensitivity, and the required final product quality.
The second step is vessel evaluation. The engineer should consider tank diameter, straight-side height, bottom shape, internal coils, baffles, outlet configuration, available nozzle size, mounting flange, and drainability. A bottom-entry mixer must be positioned so that its impeller produces effective circulation without interfering with other internals.
The third step is selection of mixing intensity. High-shear operation is appropriate when the process requires agglomerate reduction, rapid wetting, fine dispersion, or emulsification. Lower-shear operation may be preferable for suspension maintenance, gentle circulation, or shear-sensitive biological materials.
The fourth step is review of cleaning and sterilization. CIP and SIP requirements should be defined at the beginning of the project. The equipment must be accessible to the cleaning medium, and the installation must avoid areas that cannot be drained, flushed, or exposed to the required sterilization conditions.
The fifth step is performance confirmation. Depending on the application, testing may evaluate mixing time, dispersion quality, particle size, emulsion stability, temperature rise, power consumption, foam generation, or solids suspension. Testing with the actual product or a representative substitute can significantly improve the reliability of the final selection.
After manufacture, commissioning should include mechanical inspection, rotation checks, motor verification, bearing review, seal and gasket inspection, control-system verification, and no-load or water-based testing where appropriate. Process trials should then be conducted under controlled conditions before routine production begins.
13. Quality Management and Documentation
Food, pharmaceutical, and biotechnology customers often require detailed equipment documentation. Typical documentation may include material certificates, dimensional records, welding records, surface-finish information, pressure or leak test records, motor data, component manuals, assembly drawings, inspection reports, and cleaning or sterilization recommendations.
Shiloc maintains quality management, environmental, and safety practices aligned with international business requirements. The company’s focus on traceability and internal manufacturing is intended to support reliable delivery and consistent equipment quality.
Documentation should be tailored to the customer’s validation strategy. A pharmaceutical installation may require more extensive qualification records than a general industrial mixing system. A food manufacturer may focus on hygienic material certificates, surface finish, cleanability, allergen-control procedures, and changeover validation.
Clear documentation also supports long-term maintenance. Operators can use equipment records to identify replacement bearings, gaskets, motors, gearboxes, or other components. Maintenance teams can refer to approved operating limits and inspection requirements, reducing the risk of incorrect servicing.
14. Safety and Operating Considerations
High-speed mixing equipment must be operated within its specified mechanical and process limits. The user should confirm that the motor, gearbox, coupling, bearing system, impeller, flange, and vessel structure are suitable for the selected speed and load.
The mixer should not be started under conditions that could cause excessive torque or mechanical shock. If the product is highly viscous, contains a high concentration of solids, or has settled during an extended shutdown, the start-up procedure may require special attention. The process engineer should define whether pre-dilution, lower initial speed, or a staged start is necessary.
Temperature must also be controlled. High shear can generate heat, particularly in viscous products. If the formulation is temperature-sensitive, the vessel may require cooling or a defined maximum operating time at high speed.
Foam formation should be evaluated when the product contains surfactants, proteins, or other foam-promoting ingredients. Excessive aeration can reduce product quality and may affect downstream filling or filtration. Impeller speed, liquid level, addition sequence, and vessel headspace can all influence foaming.
The magnetic coupling should be protected from operating conditions that exceed its design capability. Sudden overload, unsuitable viscosity, foreign objects, or incorrect assembly may cause decoupling or abnormal heating. Operators should follow the equipment manual and the approved operating procedure.
15. Comparison of the LMP, LHS, LHS-G, and LDC Series
The LMP series is intended for general bottom-mounted magnetic mixing. Its single-layer and multi-layer designs support suspension, dissolution, dispersion, and solution preparation. The LMP-D multi-layer configuration can improve circulation in larger or more complex vessels and is identified for cell reactor applications.
The LHS series provides higher speed than the LMP models and is designed for low-to-moderate shear mixing. It can be used for dispersion, suspension, dissolution, and general mixing where a stronger flow field is needed but the process does not require the maximum shear intensity of the LHS-G model.
The LHS-G series is the high-shear configuration. It reaches approximately 2,850 rpm and is intended for emulsification, fine dispersion, rapid powder incorporation, and particle size reduction. Its impeller geometry and operating speed are selected for processes where localized shear is a major requirement.
The LDC series uses top-mounted magnetic drive technology. The LDC-N model reaches approximately 600 rpm and is suitable for solid-liquid mixing, dispersion, and dissolution. The LDC-W model reaches approximately 1,200 rpm and provides a higher-speed top-mounted option for dispersion, suspension, and solution tanks.
The most suitable model depends on the desired flow pattern, shear intensity, installation space, vessel design, and product characteristics. The availability of multiple configurations is an advantage because it allows the user to match the equipment to the process instead of selecting solely according to vessel volume.
16. Practical Benefits for Total Cost of Ownership
Total cost of ownership includes more than the initial equipment price. It also includes installation, utilities, cleaning time, maintenance, spare parts, product loss, downtime, validation, and the cost of quality failures. A magnetic high-shear mixer can contribute to lower lifecycle costs in several ways.
Reduced leakage risk can lower the likelihood of product loss and unplanned cleanup. Easier containment can also reduce exposure-related concerns when valuable or hazardous media are processed. The bottom-entry design may reduce building modifications where headroom is limited.
Efficient dispersion and emulsification can shorten batch processing time. Faster powder wetting and improved dissolution may reduce the need for extended recirculation or repeated processing. More uniform product quality can also reduce rejected batches and downstream corrections.
Hygienic design can contribute to shorter and more reliable cleaning cycles. If the vessel and mixer are properly designed, residues may be removed more consistently, reducing the need for manual intervention. The final result depends on cleaning validation, but the equipment’s materials and geometry provide an appropriate foundation.
Maintenance costs may also be influenced by the magnetic drive. Eliminating or reducing the use of a traditional dynamic shaft seal can reduce certain service tasks. Nevertheless, bearings, gaskets, motor components, and other parts still require planned inspection and replacement according to operating conditions.
17. Recommended Project Workflow
A successful project should begin with a complete process questionnaire. The customer should provide information about the formulation, vessel, batch size, operating temperature, viscosity, solids, cleaning agents, sterilization cycle, and desired production rate.
The equipment supplier can then recommend a preliminary mixer configuration and identify any missing data. Where the application is complex, a laboratory or pilot trial can be used to compare impeller speed, processing time, addition sequence, and final product quality.
After the technical concept is approved, the project should define the scope of supply. This may include the mixer, motor, gearbox, flange, control components, temperature or speed instrumentation, documentation, spare parts, installation support, and commissioning services.
Manufacturing should proceed under controlled quality procedures. Material identification, welding, polishing, dimensional inspection, component assembly, and functional testing should be documented. Customer-specific requirements should be reviewed before final inspection and shipment.
Once installed, the equipment should undergo commissioning and process qualification. Operators should be trained in start-up, shutdown, cleaning, inspection, troubleshooting, and emergency procedures. A preventive maintenance schedule should be established before production begins.
18. Frequently Asked Questions
What is the primary purpose of a bottom-entry high-shear magnetic emulsifier?
Its primary purpose is to provide controlled high-shear mixing for emulsification, fine dispersion, powder wetting, agglomerate reduction, dissolution, dilution, and suspension-related processes. The bottom-entry arrangement promotes circulation from the lower region of the vessel, while the magnetic drive supports contained and hygienic operation.
How does the magnetic drive reduce contamination risk?
The magnetic drive transfers rotation through a containment boundary using external and internal magnetic rotors. This reduces the need for a conventional rotating shaft seal passing through the vessel wall. As a result, the design can reduce the possibility of product leakage and external contamination, although the complete vessel and cleaning system must still be properly designed and validated.
What is the maximum speed of the high-shear model?
The LHS-G high-shear magnetic mixer reaches approximately 2,850 rpm. Other models in the product family operate at lower speeds for suspension, dissolution, general mixing, or cell-related applications.
Can the equipment process high-viscosity materials?
The equipment is suitable for applications with viscosities up to approximately 800 cP, depending on the model and process conditions. The actual selection should consider viscosity at operating temperature, non-Newtonian behavior, solids concentration, torque, batch size, and desired processing time.
What materials are used for product-contact components?
Product-contact components are manufactured from 1.4435 or 1.4404 stainless steel. These materials provide corrosion resistance and are suitable for many hygienic food, pharmaceutical, and biotechnology applications. Final material selection should be confirmed against the product and cleaning chemistry.
Why are tungsten carbide bearings used?
Tungsten carbide provides high hardness and wear resistance. It is used for the sliding bearings to support reliable operation under demanding speed and process conditions. Bearing life still depends on correct installation, lubrication or product compatibility where applicable, solids content, cleaning cycles, and operating load.
Is the mixer suitable for CIP and SIP systems?
Yes. The mixer is designed to comply with CIP/SIP requirements. However, CIP and SIP performance depends on the complete installation, including vessel geometry, flow paths, cleaning parameters, steam exposure, drainage, gasket design, and validation procedures.
Which series is best for emulsification and particle size reduction?
The LHS-G series is the primary choice for high-shear emulsification and particle size reduction. The LMP and standard LHS series are generally more suitable for suspension, dissolution, dispersion, and lower-shear mixing duties. The final selection should be based on process testing and product sensitivity.
Can the equipment be used in cell reactors?
The LMP-D multi-layer magnetic mixer is identified for cell reactor applications. The LHS-G model is intended for high-shear emulsification and may not be appropriate for shear-sensitive biological systems unless testing confirms suitability. Biological materials require careful evaluation of shear, aeration, temperature, and residence time.
What information is needed for equipment selection?
Important information includes working and maximum vessel volume, liquid density, viscosity, solids concentration, particle size, temperature, batch time, mixing objective, shear sensitivity, cleaning and sterilization requirements, vessel dimensions, and the desired final product quality.
What manufacturing support is available?
Shiloc provides equipment manufacturing, engineering and technical services, import and export support, process consultation, and customized equipment solutions. Its Shanghai facility supports processing, welding, polishing, assembly coordination, and quality control.
19. Conclusion
The Bottom-entry High-shear Magnetic Emulsifier is a specialized solution for manufacturers that require strong mixing performance without compromising hygienic design and process containment. Its combination of magnetic drive technology, bottom-mounted installation, optimized impeller geometry, stainless-steel contact parts, tungsten carbide sliding bearings, and CIP/SIP-oriented construction makes it suitable for demanding food, beverage, pharmaceutical, and biotechnology applications.
Compared with conventional mechanically sealed mixers, the equipment can reduce leakage and contamination risks while protecting valuable or sensitive media. Compared with basic agitators, it provides stronger localized shear and improved capability for powder wetting, agglomerate reduction, emulsification, and particle size control. Compared with many top-entry systems, its bottom-mounted configuration can save space above the vessel and improve access for other process connections.
The company’s strengths extend beyond the mixer itself. Shiloc (Shanghai) Industrial Trading Co., Ltd. combines European technical experience, Danish design concepts, internal manufacturing capabilities, stainless-steel processing, welding, polishing, quality control, traceability, and engineering support. This integrated approach helps customers address not only the purchase of a mixer but also the broader requirements of installation, validation, maintenance, and process optimization.
As with all process equipment, final results depend on proper model selection, vessel design, formulation properties, operating parameters, cleaning procedures, and commissioning. When these factors are evaluated together, the Bottom-entry High-shear Magnetic Emulsifier can provide a reliable and space-efficient platform for controlled particle reduction, dispersion, suspension, dissolution, and emulsification.
References
1. Supplier product information for bottom-mounted magnetic mixers and high-shear emulsification equipment.
2. General principles of hygienic design for food, pharmaceutical, and biotechnology process equipment.
3. Engineering practices for clean-in-place and steam-in-place systems.
4. Technical guidance on magnetic-drive pumps, mixers, and contained process equipment.
5. Stainless-steel material and fabrication principles for sanitary process applications.
6. Mixing fundamentals for dispersion, dissolution, suspension, emulsification, and particle size reduction.
7. Equipment selection principles for high-viscosity and solid-liquid mixing applications.
8. Quality management, traceability, welding, polishing, and inspection practices for hygienic equipment manufacturing.
Product: Bottom-entry High-shear Magnetic Emulsifier
PREV:Automatic Food Pasteurization Systems: Advanced Processing, Hygienic Design, and Reliable Shelf-Life Extension
NEXT:Sanitary Double Tube Sheet Heat Exchangers for Safe, Efficient Food and Biopharmaceutical Processing
NEXT:Sanitary Double Tube Sheet Heat Exchangers for Safe, Efficient Food and Biopharmaceutical Processing
Interested in cooperation or have questions?
Recommended LINS
✦
Food Processing Skid System
Food and Beverage Process System
Aseptic Processing Equipment for Liquid Foods
CIP Skid System for Food Industry
High Temperature Short Time Sterilizer
UHT Processing Equipment for Plant Based Milk
UHT Processing System for Dairy Products
Milk Processing Heat Exchanger
Industrial Liquid Food Sterilization Equipment
Continuous Liquid Food Sterilizer
Let'S Work Together Welcome Aboard!
-

haikexin@haikexin.com
+8613391278930
-
 +86-21-57560276
-
 No. 2819, Sihu Road,Fengxian District, Shanghai, China
Join Our Mailing List
Copyright © Shiloc (Shanghai) Industrial Trading Co., Ltd. All Rights Reserved.
Process Systems & Equipment For Food & Biopharma Manufacturers
