
 English
 русский
 Português
 Français


 Read More
Product Category
NEW Category
Contact us
Contact Us
We specialise in the research, development and manufacture of electrical wires and cables.
 +86-21-57560276
Ultra-High Temperature Tube Pasteurizer for Safe, Efficient Food and Biopharmaceutical Processing
Content
- 1 1. The Role of UHT Processing in Modern Manufacturing
- 2 2. Product Overview: Ultra-High Temperature Tube Pasteurizer
- 3 3. How Tubular UHT Technology Works
- 4 4. Core Advantages of the Tube Pasteurizer
- 4.1 4.1 Consistent and Controllable Thermal Treatment
- 4.2 4.2 Suitability for a Broad Product Range
- 4.3 4.3 Reduced Product Exposure and Hygienic Flow Paths
- 4.4 4.4 Energy Efficiency Through Heat Recovery
- 4.5 4.5 Continuous Operation and Production Flexibility
- 4.6 4.6 Easier Integration With Automated Plants
- 5 5. Comparison With Alternative Heating Systems
- 6 6. Hygienic and Sanitary Design Principles
- 7 7. Advanced Manufacturing Processes and Engineering Strengths
- 8 8. Process Control, Safety, and Validation
- 9 9. Applications in Food and Beverage Manufacturing
- 10 10. Considerations for Biopharmaceutical and Related Industries
- 11 11. Installation, Operation, and Maintenance
- 12 12. Selecting the Right UHT Tube Pasteurizer
- 13 13. Why Choose a Process-Focused Equipment Partner
- 14 14. Sustainability and Long-Term Operating Value
- 15 15. Future Development of Tube-Based UHT Systems
- 16 16. Frequently Asked Questions
- 16.1 What is an Ultra-High Temperature Tube Pasteurizer?
- 16.2 How is a tubular system different from a plate heat exchanger?
- 16.3 Can the pasteurizer process products with particles?
- 16.4 Does the system reduce energy consumption?
- 16.5 Is the system suitable for biopharmaceutical manufacturing?
- 16.6 How is hygienic design achieved?
- 16.7 What manufacturing capabilities support the equipment?
- 16.8 Can the pasteurizer be customized?
- 16.9 What information should a customer provide for a quotation?
- 16.10 What support may be required after delivery?
- 17 Conclusion
- 18 References
- 19 Product: Ultra-High Temperature Tube Pasteurizer (UHT)
Ultra-high temperature processing has become one of the most important technologies for manufacturers that need reliable microbial control, extended product stability, and efficient continuous production. In food and beverage plants, UHT treatment supports the manufacture of shelf-stable milk, cream, plant-based drinks, liquid nutrition products, sauces, desserts, and other sensitive formulations. In biopharmaceutical and related industries, controlled thermal treatment may also be used for selected process fluids, buffers, media components, and non-sterile liquid preparation steps where the product and process conditions permit.
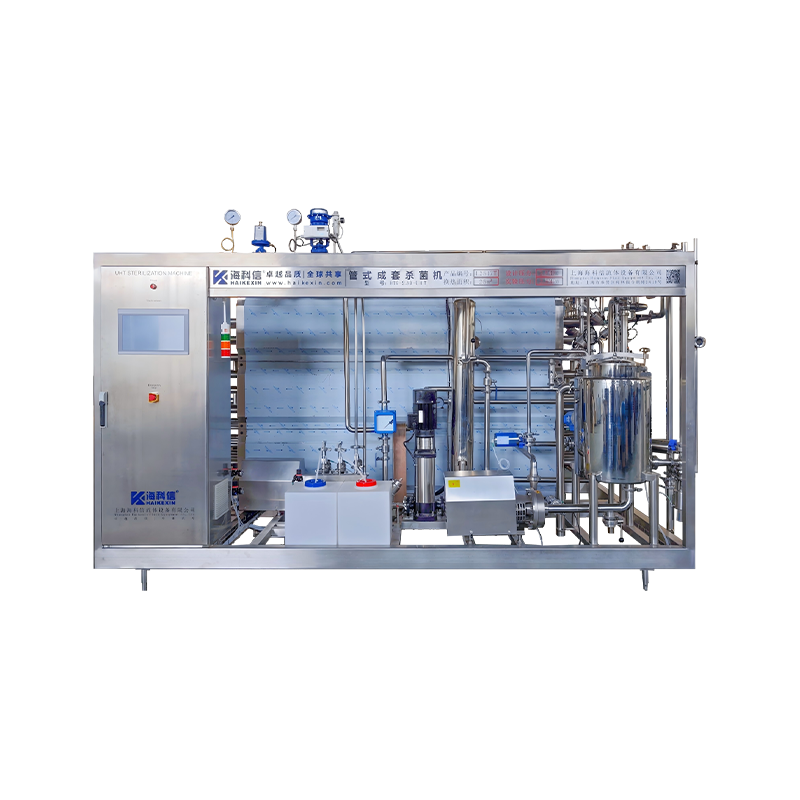
The Ultra-High Temperature Tube Pasteurizer (UHT) is designed for manufacturers that require a controlled, hygienic, and adaptable heating system. Its tubular heat-transfer configuration provides a practical solution for products with different viscosities, suspended particles, and fouling characteristics. Compared with less flexible heating systems, a properly engineered tube pasteurizer can offer dependable heat treatment, reduced product exposure, simplified cleaning, and more consistent process control.
This article explains the working principles, technical advantages, hygienic design features, manufacturing strengths, application possibilities, and selection considerations associated with an advanced tube-based UHT system. It also examines how Shiloc (Shanghai) Industrial Trading Co., Ltd. supports food, beverage, biopharmaceutical, daily chemical, and fine chemical manufacturers through European know-how, Danish design principles, process engineering capability, and controlled equipment manufacturing in Shanghai.
1. The Role of UHT Processing in Modern Manufacturing
UHT processing uses a carefully controlled combination of temperature and holding time to reduce microorganisms and improve the storage stability of liquid products. The treatment is normally performed in a continuous system rather than in individual containers. Product flows through a heating section, reaches the required treatment temperature, remains under controlled conditions for a defined period, and is then cooled before downstream filling, blending, or packaging.
The main objective is not simply to heat a product. A successful UHT process must deliver the required microbiological effect while protecting flavor, color, nutritional value, texture, and functional properties. Excessive heating can cause cooked flavors, protein changes, sediment formation, viscosity shifts, or loss of sensitive ingredients. Insufficient heating can compromise product safety and shelf life. The engineering challenge is therefore to achieve the correct thermal profile repeatedly and efficiently.
Tube pasteurizers are well suited to this challenge because the product travels through a controlled flow path while heat is transferred through the walls of sanitary tubes. The design can be adapted to the characteristics of the product, the required throughput, the treatment temperature, the holding time, and the cleaning strategy. A complete system may include product balance tanks, pumps, regenerative heat exchangers, heating sections, holding tubes, cooling sections, valves, instruments, control panels, and clean-in-place connections.
For manufacturers, the value of UHT technology extends beyond microbial reduction. A stable process can reduce product losses, improve production planning, support longer distribution distances, and make it possible to supply products without continuous refrigeration when the formulation, packaging, and validated process allow it. These benefits are particularly important for international supply chains and markets where cold-chain infrastructure is limited or expensive.
2. Product Overview: Ultra-High Temperature Tube Pasteurizer
The Ultra-High Temperature Tube Pasteurizer is a continuous thermal processing system based on tubular heat exchange. Product enters the system through a controlled inlet and is conveyed through a sequence of treatment zones. Depending on the process design, these zones may include preheating, regeneration, final heating, holding, cooling, and final chilling or aseptic transfer.
The tubular arrangement can be configured for a wide range of liquid products. It is particularly useful when a product contains fibers, particles, suspended solids, proteins, oils, or moderate-to-high viscosity. Tube diameter, tube length, flow velocity, pump selection, and heat-transfer surface can be selected according to the product and production target. This makes the system more adaptable than a standardized heating unit designed for only one narrow product category.
A typical operating sequence begins with product supply from a balance tank. A sanitary pump moves the product into the heat exchanger. In a regenerative section, hot treated product can transfer part of its energy to incoming cold product, reducing the external heating and cooling load. The product then passes through the final heating zone, where steam, hot water, or another approved heating medium raises it to the target temperature. It enters the holding tube for the required residence time before moving through the cooling section.
Where the application requires it, the system can incorporate diversion logic. If the temperature, flow rate, pressure, or another critical parameter falls outside the approved range, the product can be diverted away from the treated-product outlet. This type of protection helps prevent under-processed material from entering the finished-product stream. The precise control philosophy should be established during process design and validated for the individual product.
The equipment can also be integrated with upstream formulation and downstream filling systems. It may be connected to mixing tanks, homogenizers, deaeration units, sterile tanks, filling machines, storage vessels, or transfer skids. This makes the pasteurizer more than an isolated heating machine: it becomes a central component of a complete process line.
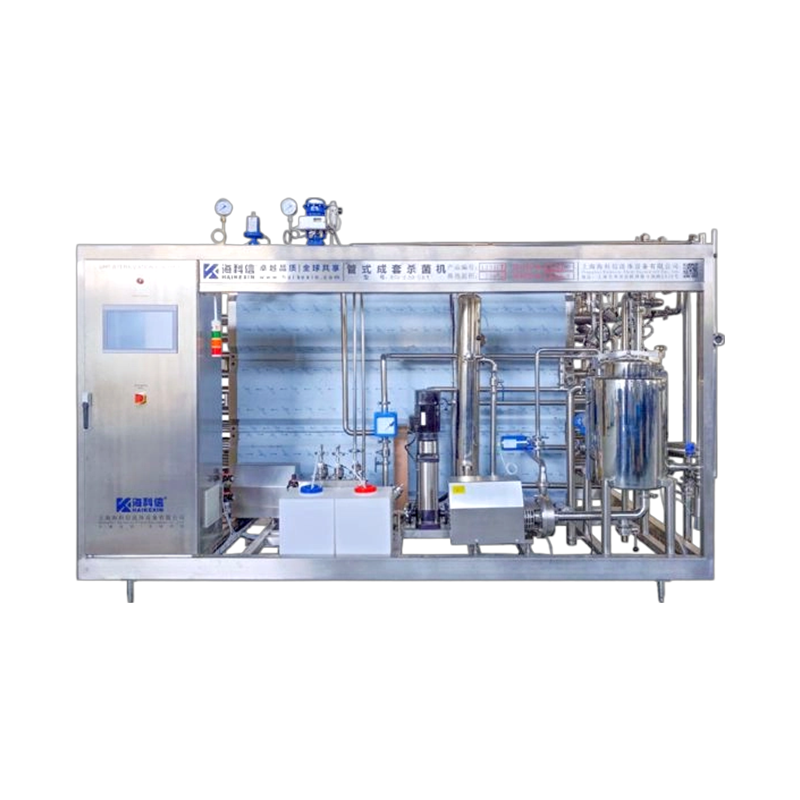
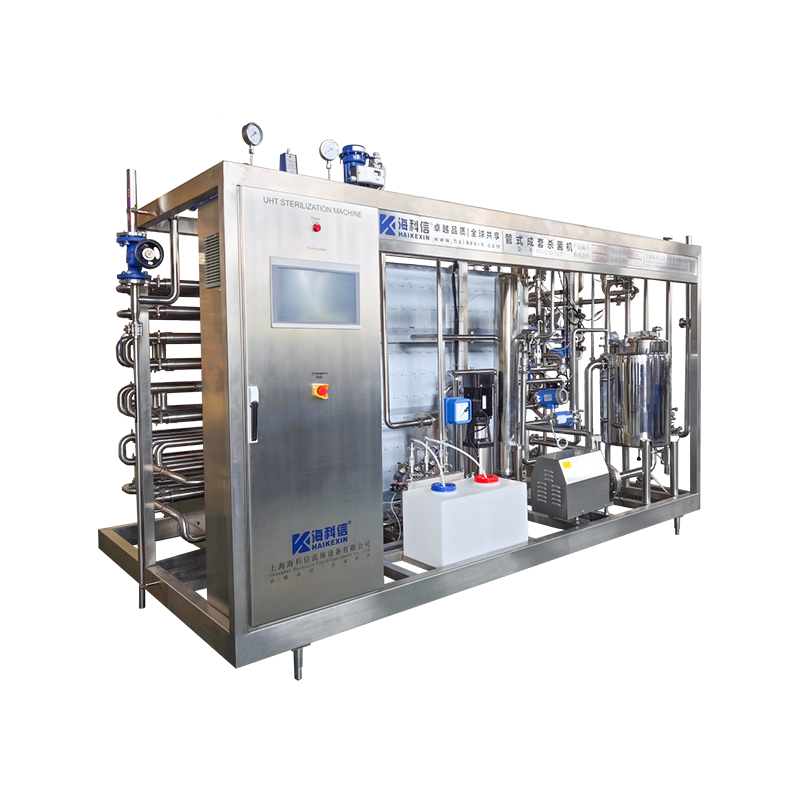
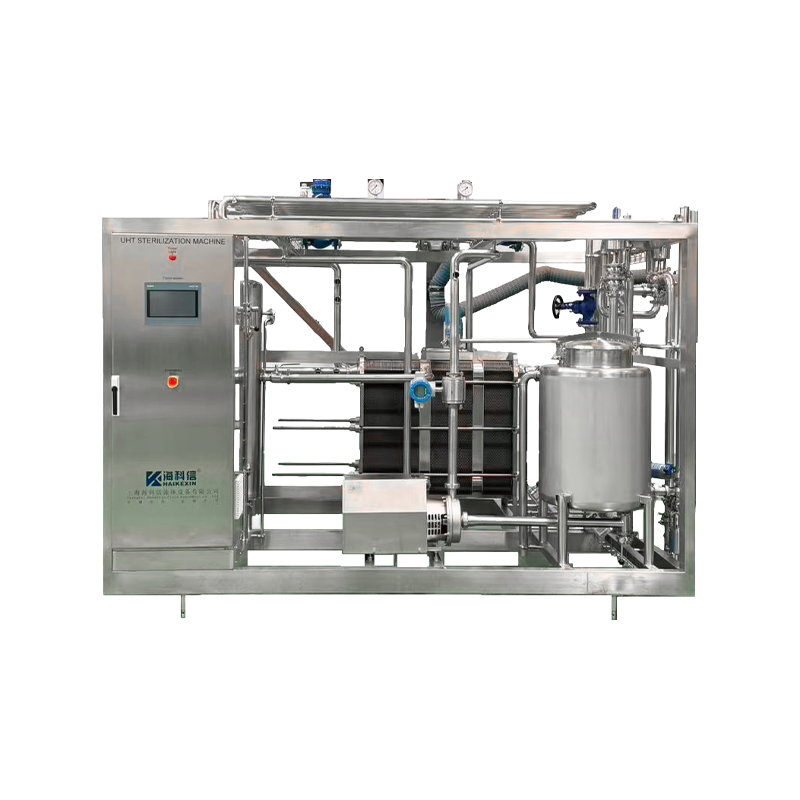
Ultra-High Temperature Tube Pasteurizer (UHT)
3. How Tubular UHT Technology Works
3.1 Product Flow and Heat Transfer
In a tubular heat exchanger, the product flows through one side of a series of sanitary tubes while the heating or cooling medium flows around the tubes or through a separate channel. Heat passes through the tube wall. The product does not directly contact the heating medium, which supports hygienic separation and gives the process engineer better control over the treatment conditions.
The amount of heat transferred depends on several factors, including the temperature difference between the product and utility medium, the available heat-transfer area, product velocity, viscosity, tube geometry, and the physical properties of the product. Proper sizing is essential. A system that is too small may fail to achieve the required heating rate or production capacity. A system that is unnecessarily large may increase capital cost, cleaning requirements, and energy consumption.
For products with higher viscosity, the system must be designed to maintain stable flow and avoid excessive pressure drop. Pump selection, tube diameter, bends, valves, and internal surface finish all influence performance. For products containing particles, the tubes must provide sufficient passage area and gentle handling to reduce blockage or particle damage. For protein-rich or sugar-containing products, the heating profile must be carefully controlled to reduce fouling.
3.2 Regenerative Heating and Cooling
Regeneration is one of the most important energy-saving features available in many UHT systems. In a regenerative section, the incoming product is warmed by the outgoing hot product, while the treated product is partially cooled by the incoming product. This internal energy exchange lowers the amount of external steam or hot water needed for heating and reduces the demand for cooling utilities.
Regeneration can improve operating economics without compromising the treatment principle. It may also reduce the thermal shock experienced by the product because the temperature changes can be distributed across multiple stages. The final heating and final cooling sections then provide the precise adjustment required to reach the validated process conditions.
The practical level of regeneration depends on product properties, process configuration, hygiene requirements, pressure relationships, and cleaning design. A skilled process engineering team must balance energy recovery with the need to avoid cross-contamination, maintain positive pressure relationships, and support effective cleaning.
3.3 Holding Time and Process Stability
The holding tube provides the time required for the product to remain at or above the specified treatment condition. Holding time is influenced by tube length, internal diameter, flow rate, temperature, and the flow profile. It is not enough to calculate a nominal residence time without considering the actual operating behavior of the system.
Process stability depends on accurate instruments and repeatable fluid movement. Temperature sensors, pressure transmitters, flowmeters, control valves, and programmable control logic work together to monitor and regulate the treatment. Changes in flow rate can change residence time. Changes in viscosity can affect pump load and heat transfer. Changes in utility pressure can influence the heating response. For this reason, a UHT system should be designed as an integrated process rather than as a collection of unrelated components.
4. Core Advantages of the Tube Pasteurizer
4.1 Consistent and Controllable Thermal Treatment
The principal advantage of the Ultra-High Temperature Tube Pasteurizer is its ability to deliver a controlled thermal profile. Product moves continuously through defined heating and holding zones, allowing the manufacturer to establish repeatable operating parameters. This consistency is essential for food safety, product quality, regulatory compliance, and production planning.
Compared with less controlled batch heating methods, a continuous tubular system can reduce variations between batches. It can also lower the risk of localized overheating that may occur when a product is heated unevenly in a vessel. When paired with suitable instruments and automation, the system provides operators with clear information about temperature, pressure, flow, and system status.
4.2 Suitability for a Broad Product Range
Tubular systems can be engineered for products that are difficult to process in narrow-channel or plate-based systems. Depending on the tube configuration, they may handle products containing pulp, fibers, suspended particles, proteins, oils, and moderate viscosity. This versatility is valuable for manufacturers that produce multiple product families on one site.
Potential food and beverage applications include dairy beverages, flavored milk, cream products, plant-based beverages, liquid meal replacements, fruit preparations, sauces, soups, desserts, and nutritional drinks. Each application requires its own process study. A formulation containing particulates will not have the same requirements as a low-viscosity beverage, and a protein-rich liquid may require a different heating strategy from a sugar-based sauce.
In biopharmaceutical and biotechnology-related operations, the equipment may be considered for selected liquid process streams where thermal treatment is appropriate. Possible examples include certain buffers, media components, process water-related preparations, or non-sensitive liquid intermediates. Suitability must always be confirmed by the responsible process, quality, and validation teams because many biological products are heat-sensitive and cannot be treated using conventional UHT conditions.
4.3 Reduced Product Exposure and Hygienic Flow Paths
A closed tubular flow path can reduce the product’s exposure to the surrounding environment during treatment. Sanitary connections, hygienic valves, polished product-contact surfaces, appropriate drainage, and controlled pressure relationships help reduce contamination risks. The design should avoid unnecessary dead legs, difficult-to-clean pockets, and stagnant zones.
Hygienic engineering is especially important when the same equipment is used for products with different ingredients or allergen profiles. A well-designed system can support effective cleaning and changeover, helping manufacturers reduce downtime and protect product integrity. The exact hygienic standard, surface finish, elastomer selection, and validation procedure should be determined according to the application and applicable regulations.
4.4 Energy Efficiency Through Heat Recovery
Energy consumption is a major operating cost in thermal processing. Regenerative heat exchange can reduce the demand for external heating and cooling. By recovering energy from the treated product, the system can improve utility efficiency while maintaining the required product temperature profile.
Energy efficiency also depends on insulation, proper utility control, short and logical piping arrangements, pump efficiency, and the operating schedule. A supplier with process engineering capability can evaluate the complete system rather than focusing only on the heat exchanger. This broader approach can identify opportunities to reduce steam consumption, cooling-water demand, heat loss, and unnecessary pumping.
4.5 Continuous Operation and Production Flexibility
Continuous operation can improve production capacity and reduce the labor associated with repeated batch charging and discharge. Once the system reaches stable operating conditions, product can be processed at a consistent rate. This supports larger production runs and more predictable downstream filling.
The equipment can also be designed for different capacities and product recipes. Modular arrangements may allow a manufacturer to begin with one production requirement and expand later. The selection of holding sections, pump capacity, heat-transfer area, controls, and connection points should consider future production needs as well as current demand.
4.6 Easier Integration With Automated Plants
Modern manufacturers expect process equipment to communicate with plant control systems and support traceable production records. The tube pasteurizer can be equipped with sensors, control logic, alarms, data recording, and recipe management according to project requirements. Automation may reduce operator dependency, improve repeatability, and support investigations when deviations occur.
Automation does not replace process validation or skilled operators. Instead, it gives operators better tools to observe and manage the process. Critical control points, alarm limits, interlocks, and product diversion logic should be documented and tested during commissioning.
5. Comparison With Alternative Heating Systems
| Evaluation Area | Tubular UHT Pasteurizer | Batch Heating Vessel | Plate Heat Exchanger |
|---|---|---|---|
| Operating mode | Continuous processing with controlled heating and holding | Batch-based heating and cooling | Continuous processing through narrow plate channels |
| Product flexibility | Suitable for many liquids, including selected viscous or particulate products | Flexible for recipes but often slower and more labor-intensive | Highly effective for clean, low-viscosity liquids with suitable flow behavior |
| Heat recovery | Can include regenerative heating and cooling | Usually limited unless additional recovery equipment is installed | Often provides strong heat recovery capability |
| Particle handling | Can be designed with larger passages and suitable tube geometry | Can handle particles, depending on agitator and vessel design | May be limited by channel size and risk of blockage |
| Fouling considerations | Managed through velocity, temperature profile, surface finish, and cleaning design | May experience deposits on vessel surfaces and heating jackets | May be sensitive to fouling in narrow channels |
| Scalability | Can be configured for different capacities and process conditions | Capacity increases may require larger vessels or additional batches | Scalable for compatible products and operating ranges |
| Cleaning approach | Designed for automated clean-in-place circulation | Requires vessel, agitator, spray device, and connected piping cleaning | Designed for clean-in-place but requires careful control of pressure and flow |
| Typical strength | Versatility, robust flow path, and suitability for challenging liquids | Recipe flexibility and simple batch process management | Compact heat transfer for compatible low-viscosity products |
No one heat exchanger is ideal for every application. A plate system may be highly efficient for a clean, low-viscosity beverage, while a tubular system may provide greater confidence for a product with particles or a higher tendency to foul narrow passages. A batch vessel may be appropriate for small-scale or highly variable recipes, but a continuous UHT line can offer superior throughput and repeatability for larger production volumes.
The correct comparison should include product composition, target capacity, thermal sensitivity, cleaning requirements, available utilities, installation space, labor, validation expectations, and future expansion. The tube pasteurizer’s advantage is not that it replaces every other technology, but that it offers a balanced combination of flexibility, hygienic design, continuous operation, and process control.
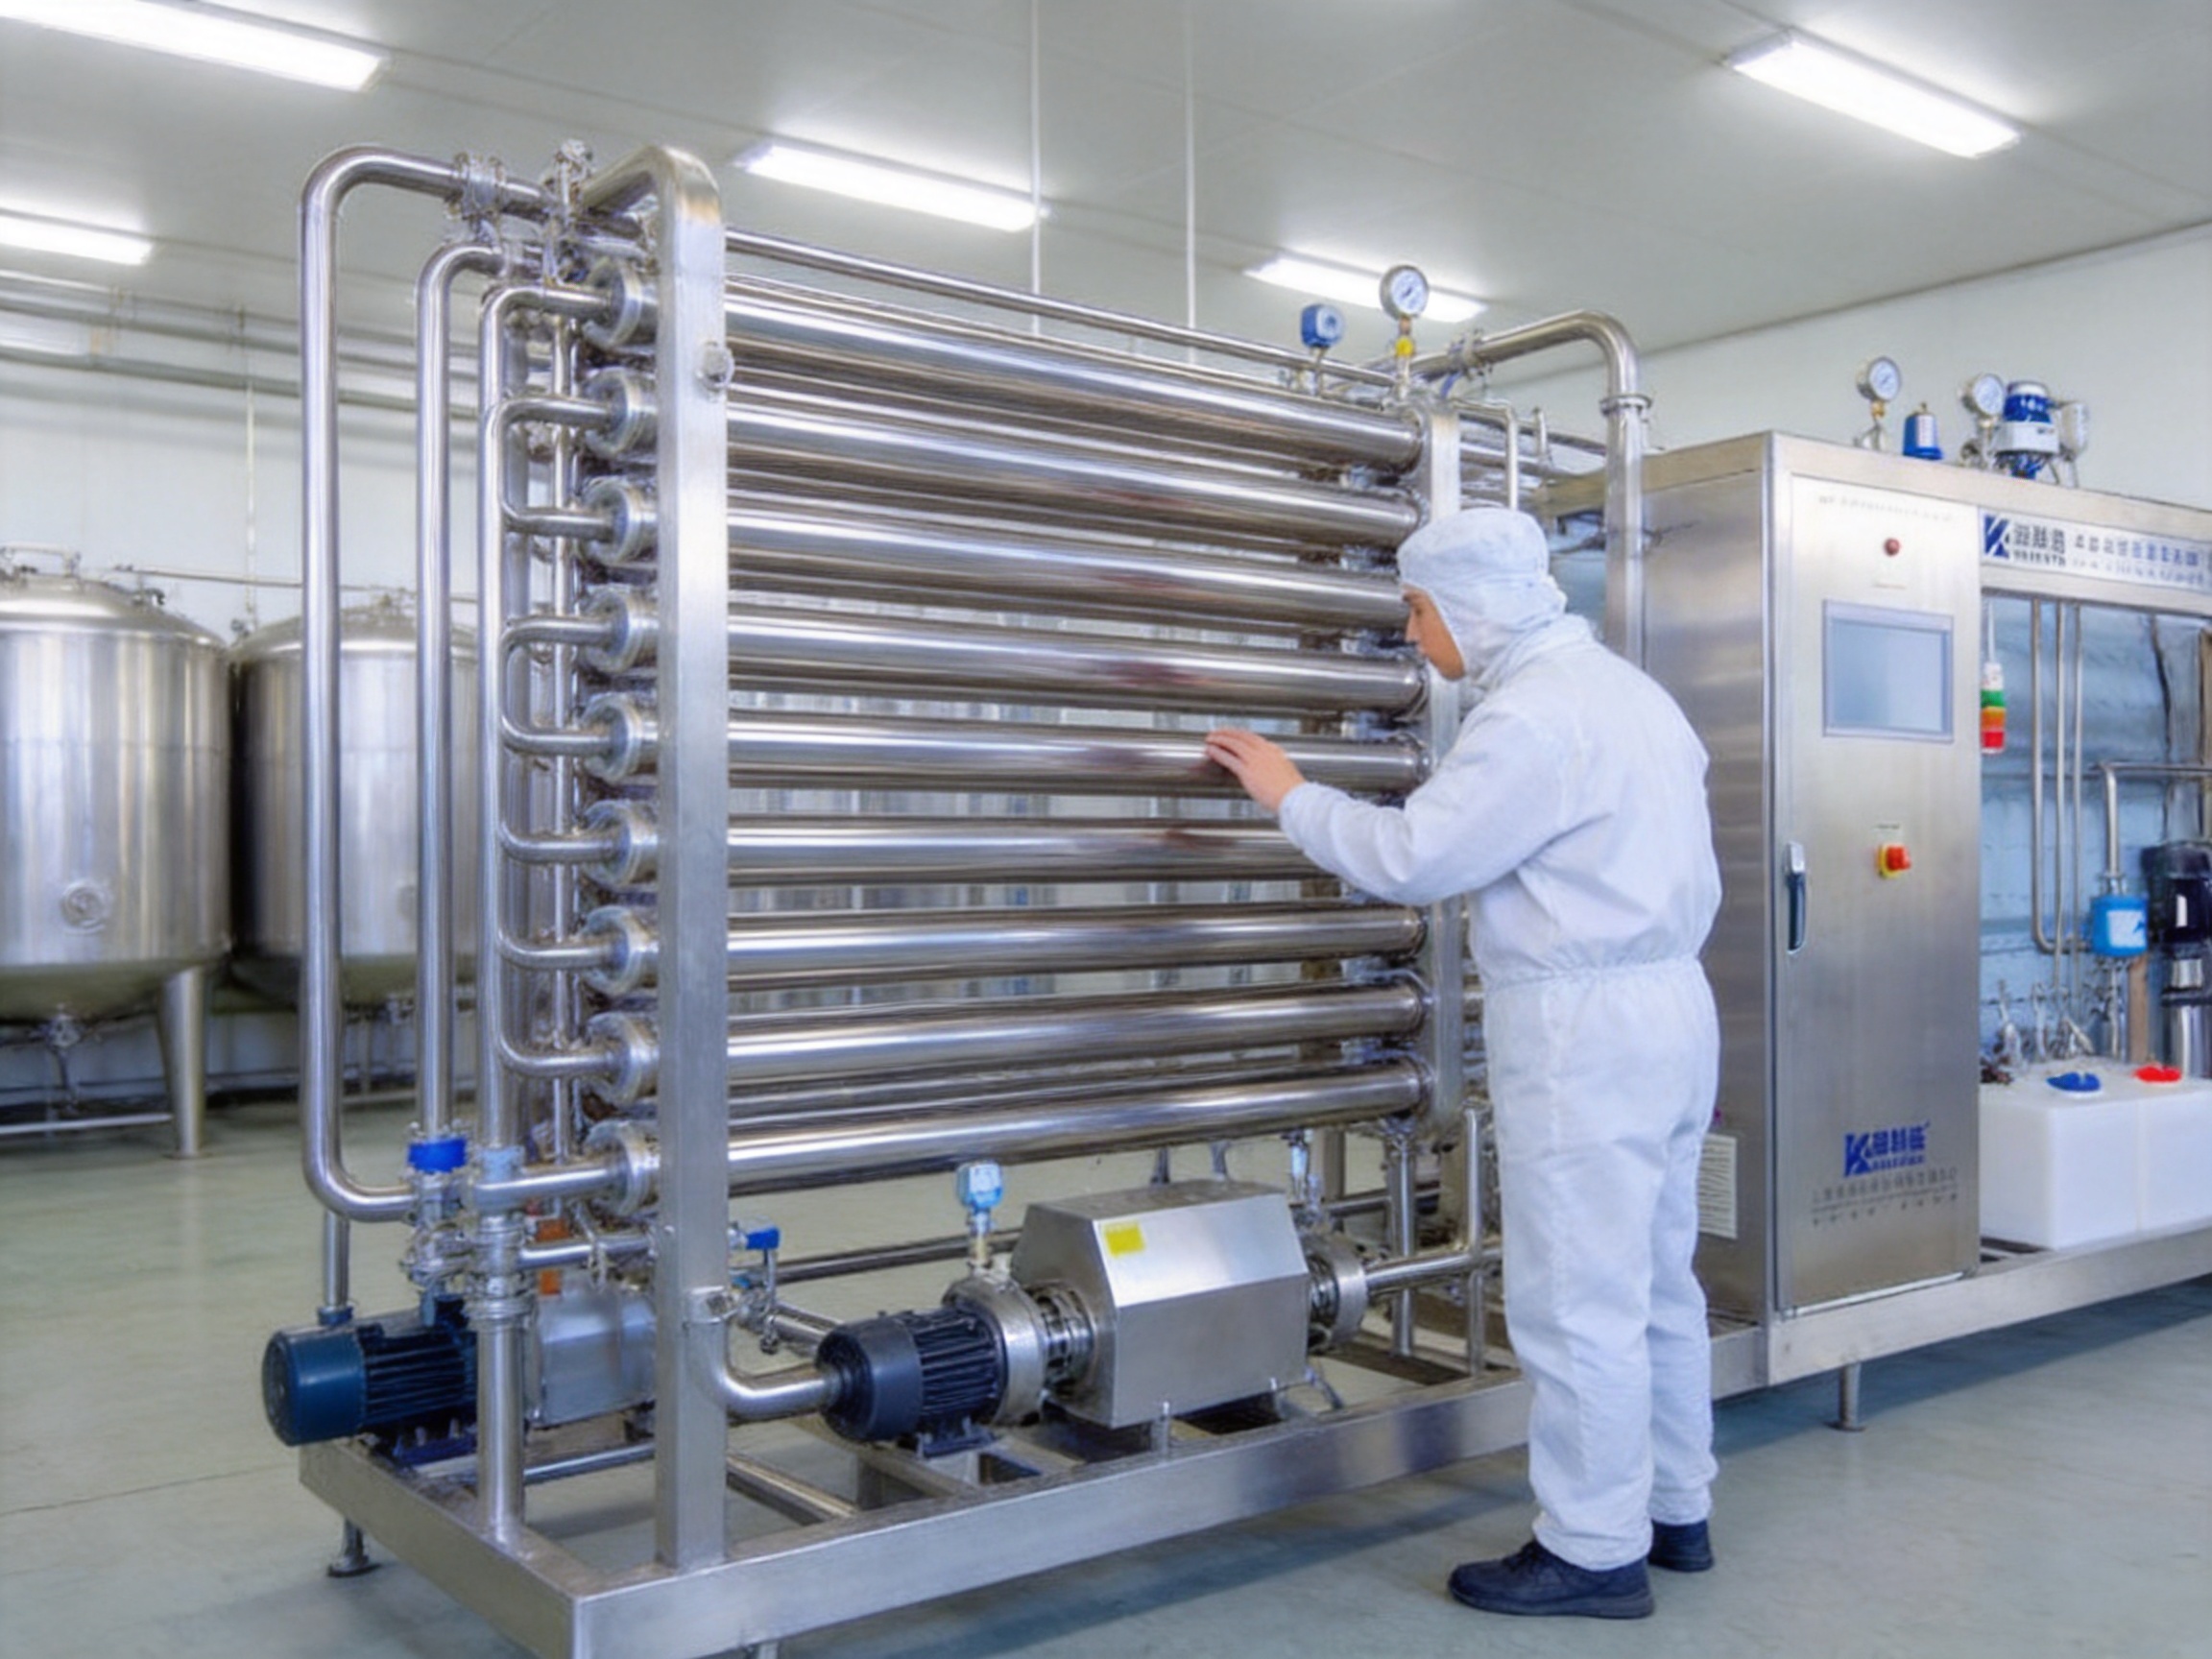
6. Hygienic and Sanitary Design Principles
Hygienic design begins with the product-contact path. Surfaces should be compatible with the product, cleaning chemicals, process temperature, and operating pressure. Stainless steel is commonly selected for sanitary process equipment because of its corrosion resistance, durability, cleanability, and established use in food and pharmaceutical environments. The precise grade and finish should be selected according to the application and relevant standards.
Welds in the product-contact area should be made using controlled procedures and finished to the specified hygienic quality. Poorly executed welds can create crevices, rough areas, or corrosion points that trap product and reduce cleaning effectiveness. Tube alignment, gasket compression, valve orientation, and drainability are also important parts of sanitary construction.
A hygienic system should minimize dead legs and areas where product can remain after production. Piping should be arranged to support drainage, and components should be accessible for inspection and maintenance. The design should distinguish between product-contact areas and utility areas so that contamination risks are controlled.
Gaskets, seals, valve seats, and instrument connections require careful selection. Materials must be compatible with the product and cleaning regime. Seal degradation can create leaks, particles, or contamination risks. Preventive maintenance plans should include inspection and replacement intervals for wear components.
Clean-in-place capability is a central consideration. A typical cleaning program may involve a pre-rinse, alkaline wash, intermediate rinse, acid wash where required, final rinse, and sanitization step. The actual sequence depends on the product residues, equipment materials, cleaning chemicals, temperature, flow velocity, and validation requirements. The system must be designed so that the cleaning solution reaches all relevant surfaces with suitable turbulence and contact time.
7. Advanced Manufacturing Processes and Engineering Strengths
7.1 European Know-How and Danish Design Principles
Shiloc (Shanghai) Industrial Trading Co., Ltd. combines European process equipment know-how with Danish design principles. This approach emphasizes functional engineering, clean layouts, practical maintenance access, safe operation, efficient use of materials, and attention to the details that influence long-term reliability.
Danish and broader European equipment design traditions are often associated with strong focus on hygienic processing, operator safety, energy awareness, and lifecycle value. When these principles are applied together with local manufacturing capability, customers can receive equipment that is adapted to their process requirements while benefiting from international engineering concepts.
The design objective is not merely to produce a visually polished machine. A high-quality UHT system must perform consistently under production conditions, remain accessible for cleaning and maintenance, protect operators, and provide reliable data for process control. Engineering decisions should be based on the product, the facility, and the operating environment.
7.2 Shanghai Manufacturing Facility
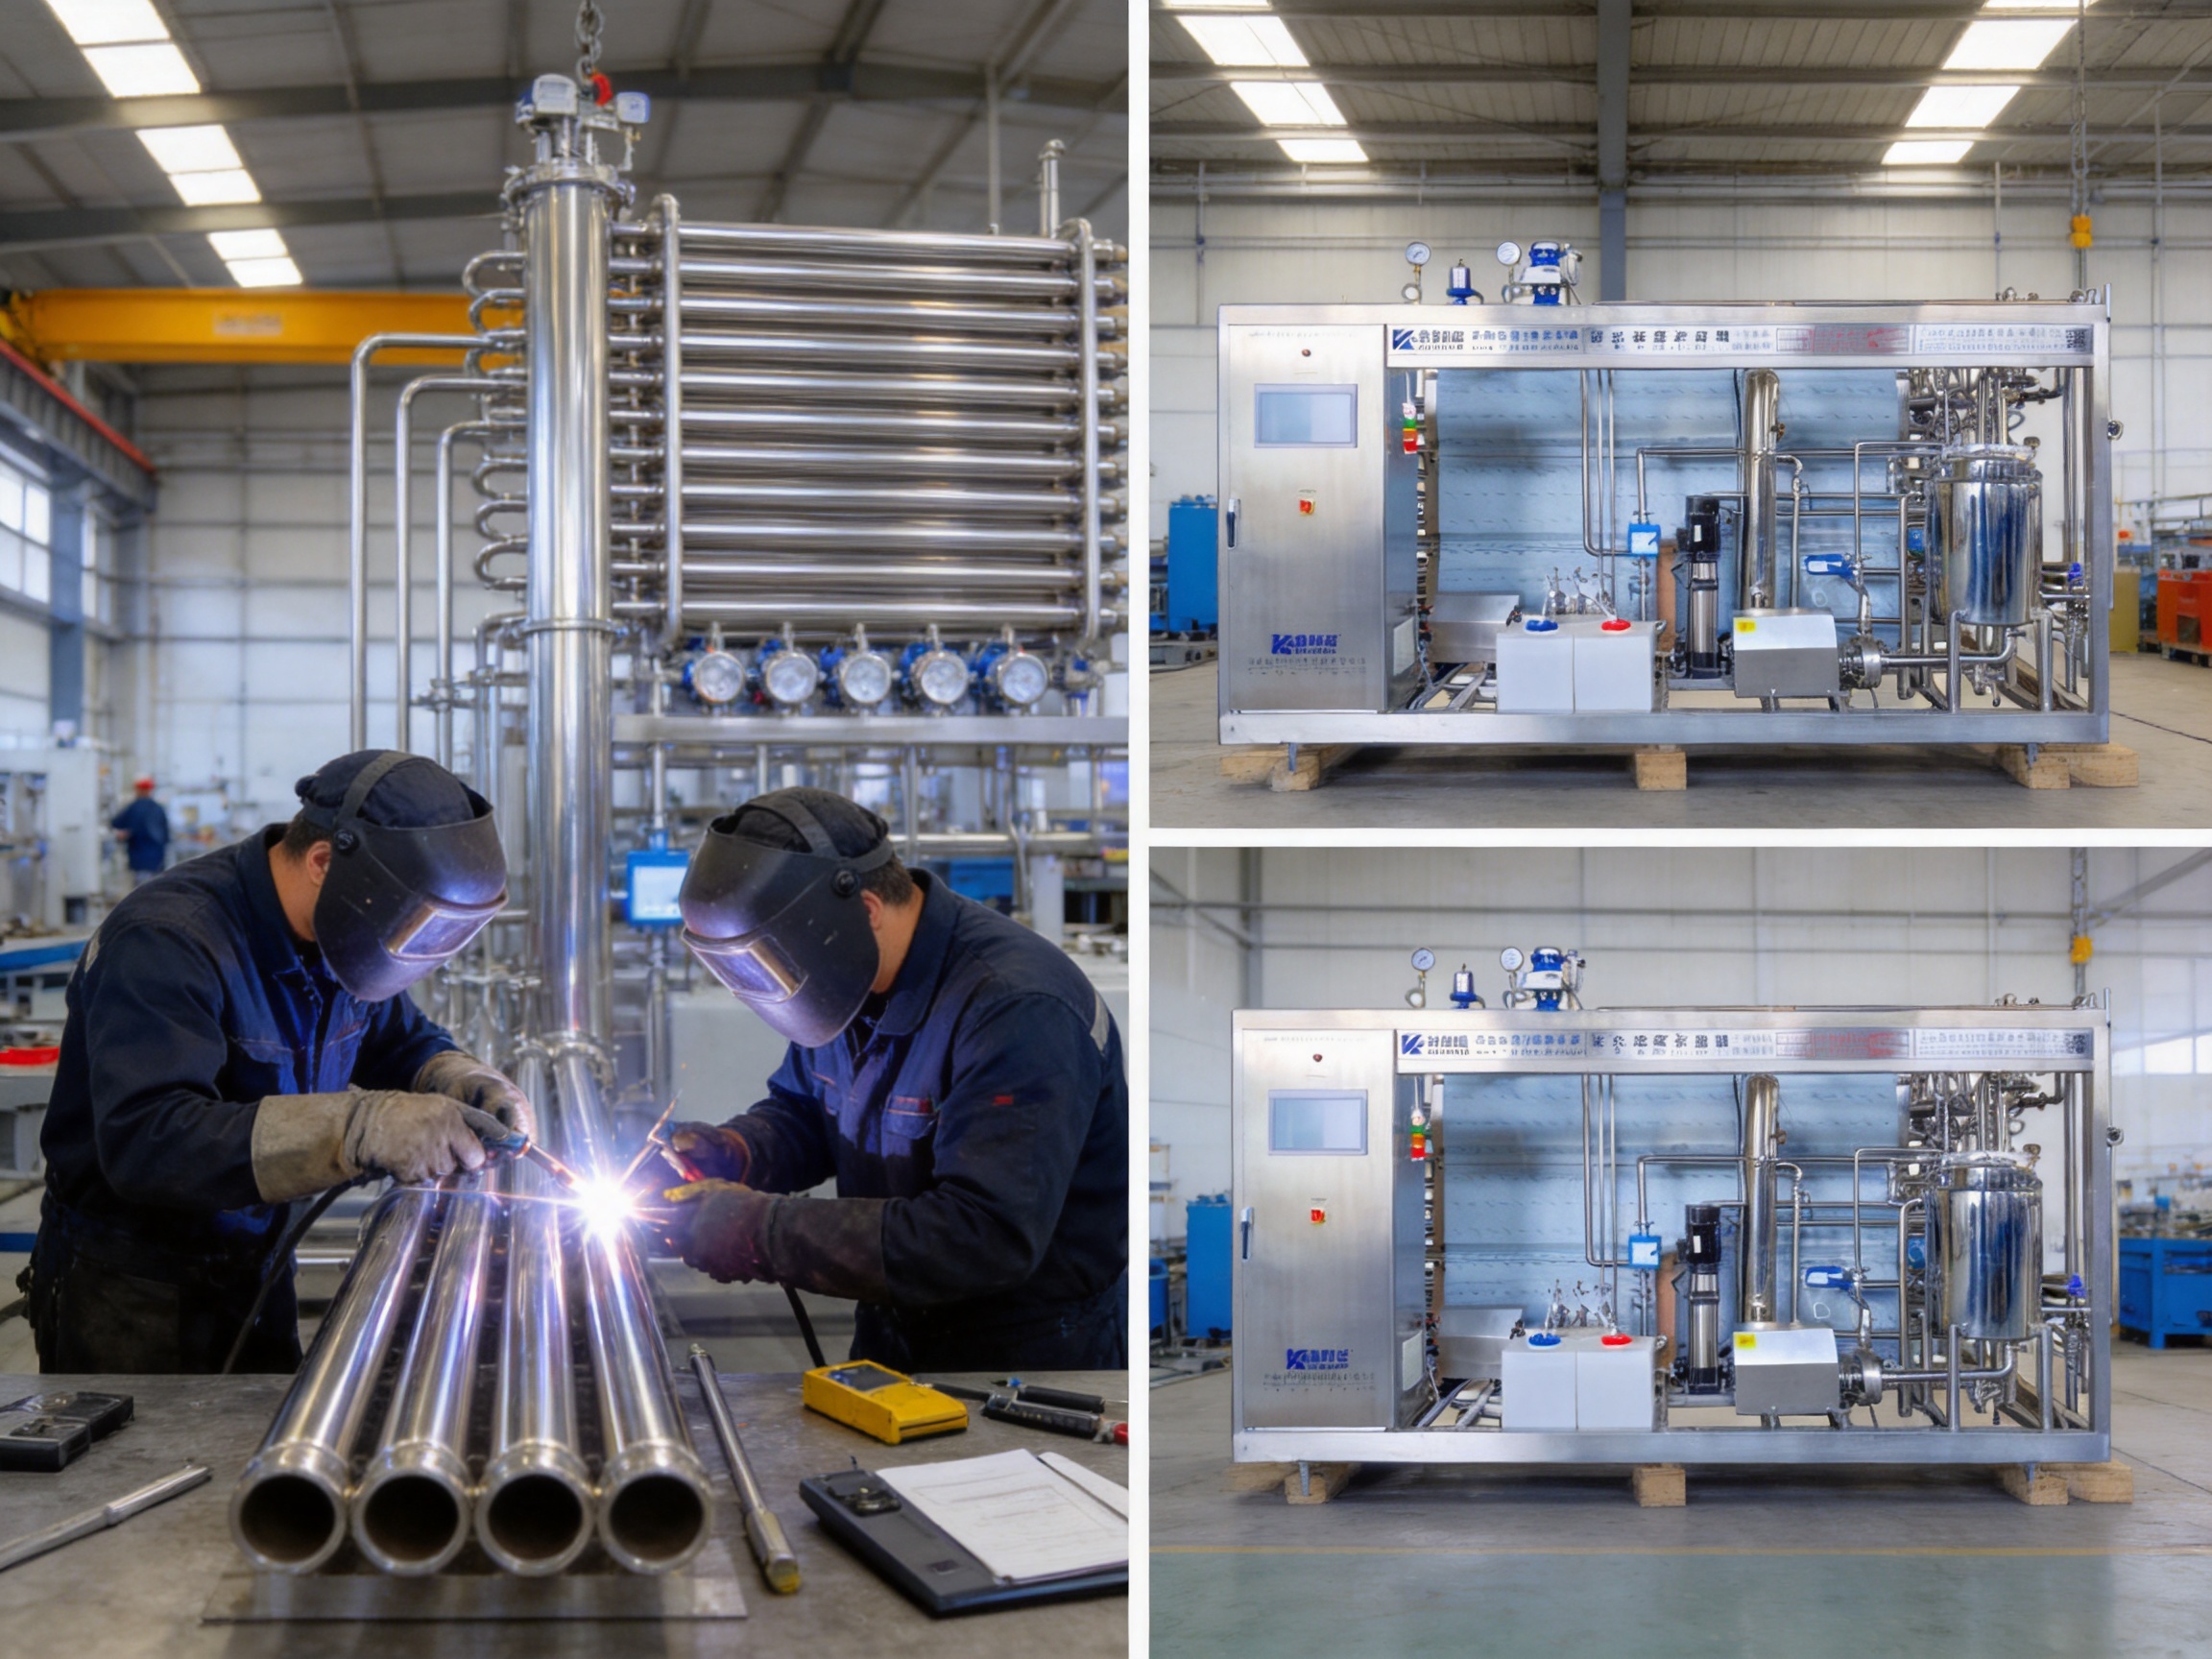
The company operates a 3,000-square-meter facility in Shanghai with capabilities covering processing, welding, polishing, and quality control. These capabilities allow important manufacturing activities to be coordinated within one organization. Better coordination can reduce communication gaps between design, fabrication, assembly, and inspection.
In sanitary equipment manufacturing, the connection between fabrication and quality control is particularly important. A design may specify a certain weld configuration, surface quality, tube arrangement, or drainability requirement. The manufacturing team must then translate that specification into a finished product that meets the intended process function. Inspection activities help confirm that the result is suitable for delivery and commissioning.
7.3 Controlled Welding and Polishing
Welding is one of the most significant manufacturing processes in a tubular pasteurizer. Product-contact welds must be made with appropriate materials, procedures, and protection. The objective is to produce joints with good mechanical strength, corrosion resistance, and cleanability.
After welding, polishing and surface finishing help create a smoother and more hygienic product-contact area. The required finish depends on the product and application. A smooth surface can reduce the opportunity for product residue to remain attached and can make cleaning more effective. Surface treatment should be controlled rather than performed only for appearance.
Manufacturing quality also depends on dimensional accuracy. Tube assemblies, support frames, valve clusters, heat exchanger connections, and skid piping must align correctly. Accurate fabrication reduces stress during installation and helps ensure that the equipment can be connected to the customer’s process line without unnecessary modification.
7.4 Process Engineering and Customization
Every UHT project should begin with a process understanding. Important questions include the product’s viscosity, particle size, density, thermal sensitivity, target flow rate, required treatment conditions, cleaning chemistry, filling method, and production schedule. The engineering team can then determine the appropriate heat-transfer arrangement, pump configuration, control philosophy, holding section, and utility requirements.
Customization may include the number of heating and cooling stages, regenerative arrangement, tube diameter, product-contact material, valve type, instrument package, skid dimensions, connection standards, and automation interface. Customization is valuable because it aligns the equipment with the actual manufacturing environment instead of forcing the customer to redesign the process around a fixed machine.
At the same time, customization should be controlled. Excessive complexity can increase cost and maintenance requirements. A strong supplier distinguishes between features that add genuine process value and features that create unnecessary complication. The best design is normally the simplest system that can reliably meet the validated process requirements.
7.5 Quality Control and Traceability
Quality control should cover incoming materials, fabrication, assembly, surface finishing, component installation, pressure testing, functional testing, and final inspection. Traceability is especially important in food and biopharmaceutical equipment because customers may need records of materials, welds, instruments, tests, and corrective actions.
Shiloc emphasizes reliable supply and traceability as part of its operating philosophy. Traceable manufacturing supports accountability throughout the project. It also helps the customer maintain documentation for internal quality systems, audits, maintenance, and future modifications.
Depending on the project, quality documentation may include material certificates, welding records, inspection reports, pressure-test results, calibration information, component certificates, surface-finish records, and factory acceptance test documentation. The exact documentation package should be agreed before production begins.
7.6 Technical Team and Project Coordination
The company has more than 20 technical specialists supporting its engineering and manufacturing activities. A multidisciplinary team can address process design, mechanical construction, hygienic details, automation, installation, commissioning, and after-sales service as connected tasks.
Strong coordination is important because thermal processing projects involve multiple interfaces. The pasteurizer must connect with product tanks, utility systems, filling equipment, cleaning systems, plant controls, and sometimes sterile barriers. Early coordination reduces the risk of incompatible connections, insufficient space, inadequate utility capacity, or difficult maintenance access.
8. Process Control, Safety, and Validation
A UHT system must be designed with process safety and equipment safety in mind. Thermal treatment involves elevated temperature, pressure, steam or hot-water utilities, moving pumps, automated valves, and chemical cleaning agents. Guards, insulation, pressure protection, emergency stops, safe access, and clear operating procedures are essential.
Instrumentation should be selected according to the criticality of the process. Temperature measurement is central, but flow, pressure, tank level, utility conditions, and valve position may also be important. Instruments should be installed where they can measure the process accurately and be maintained or calibrated without unnecessary disruption.
Control logic should define how the system starts, reaches stable conditions, transitions between products, responds to deviations, and shuts down. Interlocks may prevent unsafe operation when a pump is running without sufficient product, when a valve is in the wrong position, or when a utility condition is outside the approved range.
Validation confirms that the installed equipment and process deliver the intended result. In food manufacturing, this may include thermal validation, cleaning validation, calibration checks, and verification of diversion logic. In biopharmaceutical environments, the documentation and qualification expectations may be more extensive and must be determined by the customer’s quality system and regulatory obligations.
The supplier can support factory testing, installation assistance, commissioning, operator training, and technical documentation. However, final process approval remains the responsibility of the manufacturer and its qualified quality and production teams. The equipment supplier and end user should work together to define acceptance criteria before the project begins.
9. Applications in Food and Beverage Manufacturing
9.1 Dairy and Dairy-Based Beverages
Dairy products require careful management of heat treatment, protein stability, fouling, and flavor. A tubular system can be configured for liquid milk, flavored milk, cream, dairy drinks, and selected dessert products. The heating profile must be developed according to the fat content, protein composition, sugar level, viscosity, and packaging method.
For dairy applications, regeneration and effective cleaning can have a significant effect on operating cost. Protein and mineral deposits may develop on heated surfaces, so the system must be designed with suitable temperature control, flow velocity, surface finish, and cleaning procedures.
9.2 Plant-Based Beverages
Plant-based beverages may contain proteins, oils, fibers, starches, stabilizers, and suspended particles. Their behavior can vary significantly between formulations. Some products are prone to sedimentation, separation, or viscosity changes. A tubular UHT system can be adapted to the product’s flow characteristics and integrated with homogenization or blending stages where required.
Product development teams should evaluate the effect of heating on flavor, emulsion stability, particle size, and nutritional properties. The pasteurizer should be considered as part of the full formulation and packaging process rather than as a standalone thermal unit.
9.3 Juices, Smoothies, and Fruit Preparations
Fruit-based products may contain pulp, fibers, acids, sugars, and natural pigments. Tube diameter and pump selection are important when handling particulate products. The thermal process must achieve microbial control while limiting unwanted flavor changes and color degradation.
The equipment may be adapted for different particle levels and product textures. However, the maximum particle size, concentration, and flow behavior must be provided during design. In some cases, gentle pumping and special valve arrangements may be necessary to protect product appearance and texture.
9.4 Sauces, Soups, and Liquid Foods
Sauces and soups can range from low-viscosity liquids to highly viscous products containing solids. Tubular systems may be advantageous when the process requires a robust flow path and larger passages than those available in compact heat exchangers. Heating and cooling requirements depend on the formulation, solids content, shear sensitivity, and packaging method.
For thick products, pressure drop and pumping power must be carefully evaluated. The line should be designed to reduce unnecessary bends, restrictions, and stagnant areas. Cleaning must address fats, starches, proteins, and other residues that may adhere to the equipment.
9.5 Liquid Nutrition and Functional Drinks
Liquid nutrition products may contain proteins, minerals, vitamins, oils, carbohydrates, and specialty ingredients. Thermal treatment can affect viscosity, emulsion stability, and nutrient performance. Controlled heating and rapid cooling can help reduce unnecessary thermal exposure while achieving the specified process objective.
Manufacturers should establish clear product specifications, sampling procedures, and process limits. The pasteurizer can support repeatable treatment, but product quality also depends on ingredient preparation, mixing, homogenization, storage, and filling.
10. Considerations for Biopharmaceutical and Related Industries
Biopharmaceutical manufacturing often involves heat-sensitive products, so conventional UHT treatment is not appropriate for every application. Nevertheless, thermal processing equipment may have a role in selected support operations or in the preparation of compatible liquids. Examples may include certain process buffers, media ingredients, non-active liquid streams, or utility-related preparations, subject to technical evaluation.
For these industries, material compatibility, surface finish, drainability, documentation, cleaning, sterilization strategy, and validation are especially important. Equipment may need to support higher levels of traceability and qualification than a general food processing line. The design should be reviewed by the customer’s process development, engineering, quality, and validation departments.
The supplier’s experience with fluid equipment, aseptic mixing equipment, heat exchangers, welding, polishing, and engineering services can support the development of integrated process solutions. However, each biological or pharmaceutical application must be assessed individually. Thermal stability studies, microbiological requirements, regulatory expectations, and product-contact material specifications should be established before equipment selection.
A practical benefit of working with a supplier experienced across food, beverage, and biopharmaceutical environments is the opportunity to transfer hygienic design principles between sectors while preserving the specific compliance requirements of each industry. This cross-industry perspective can help identify robust solutions for fluid handling, cleaning, automation, and process integration.
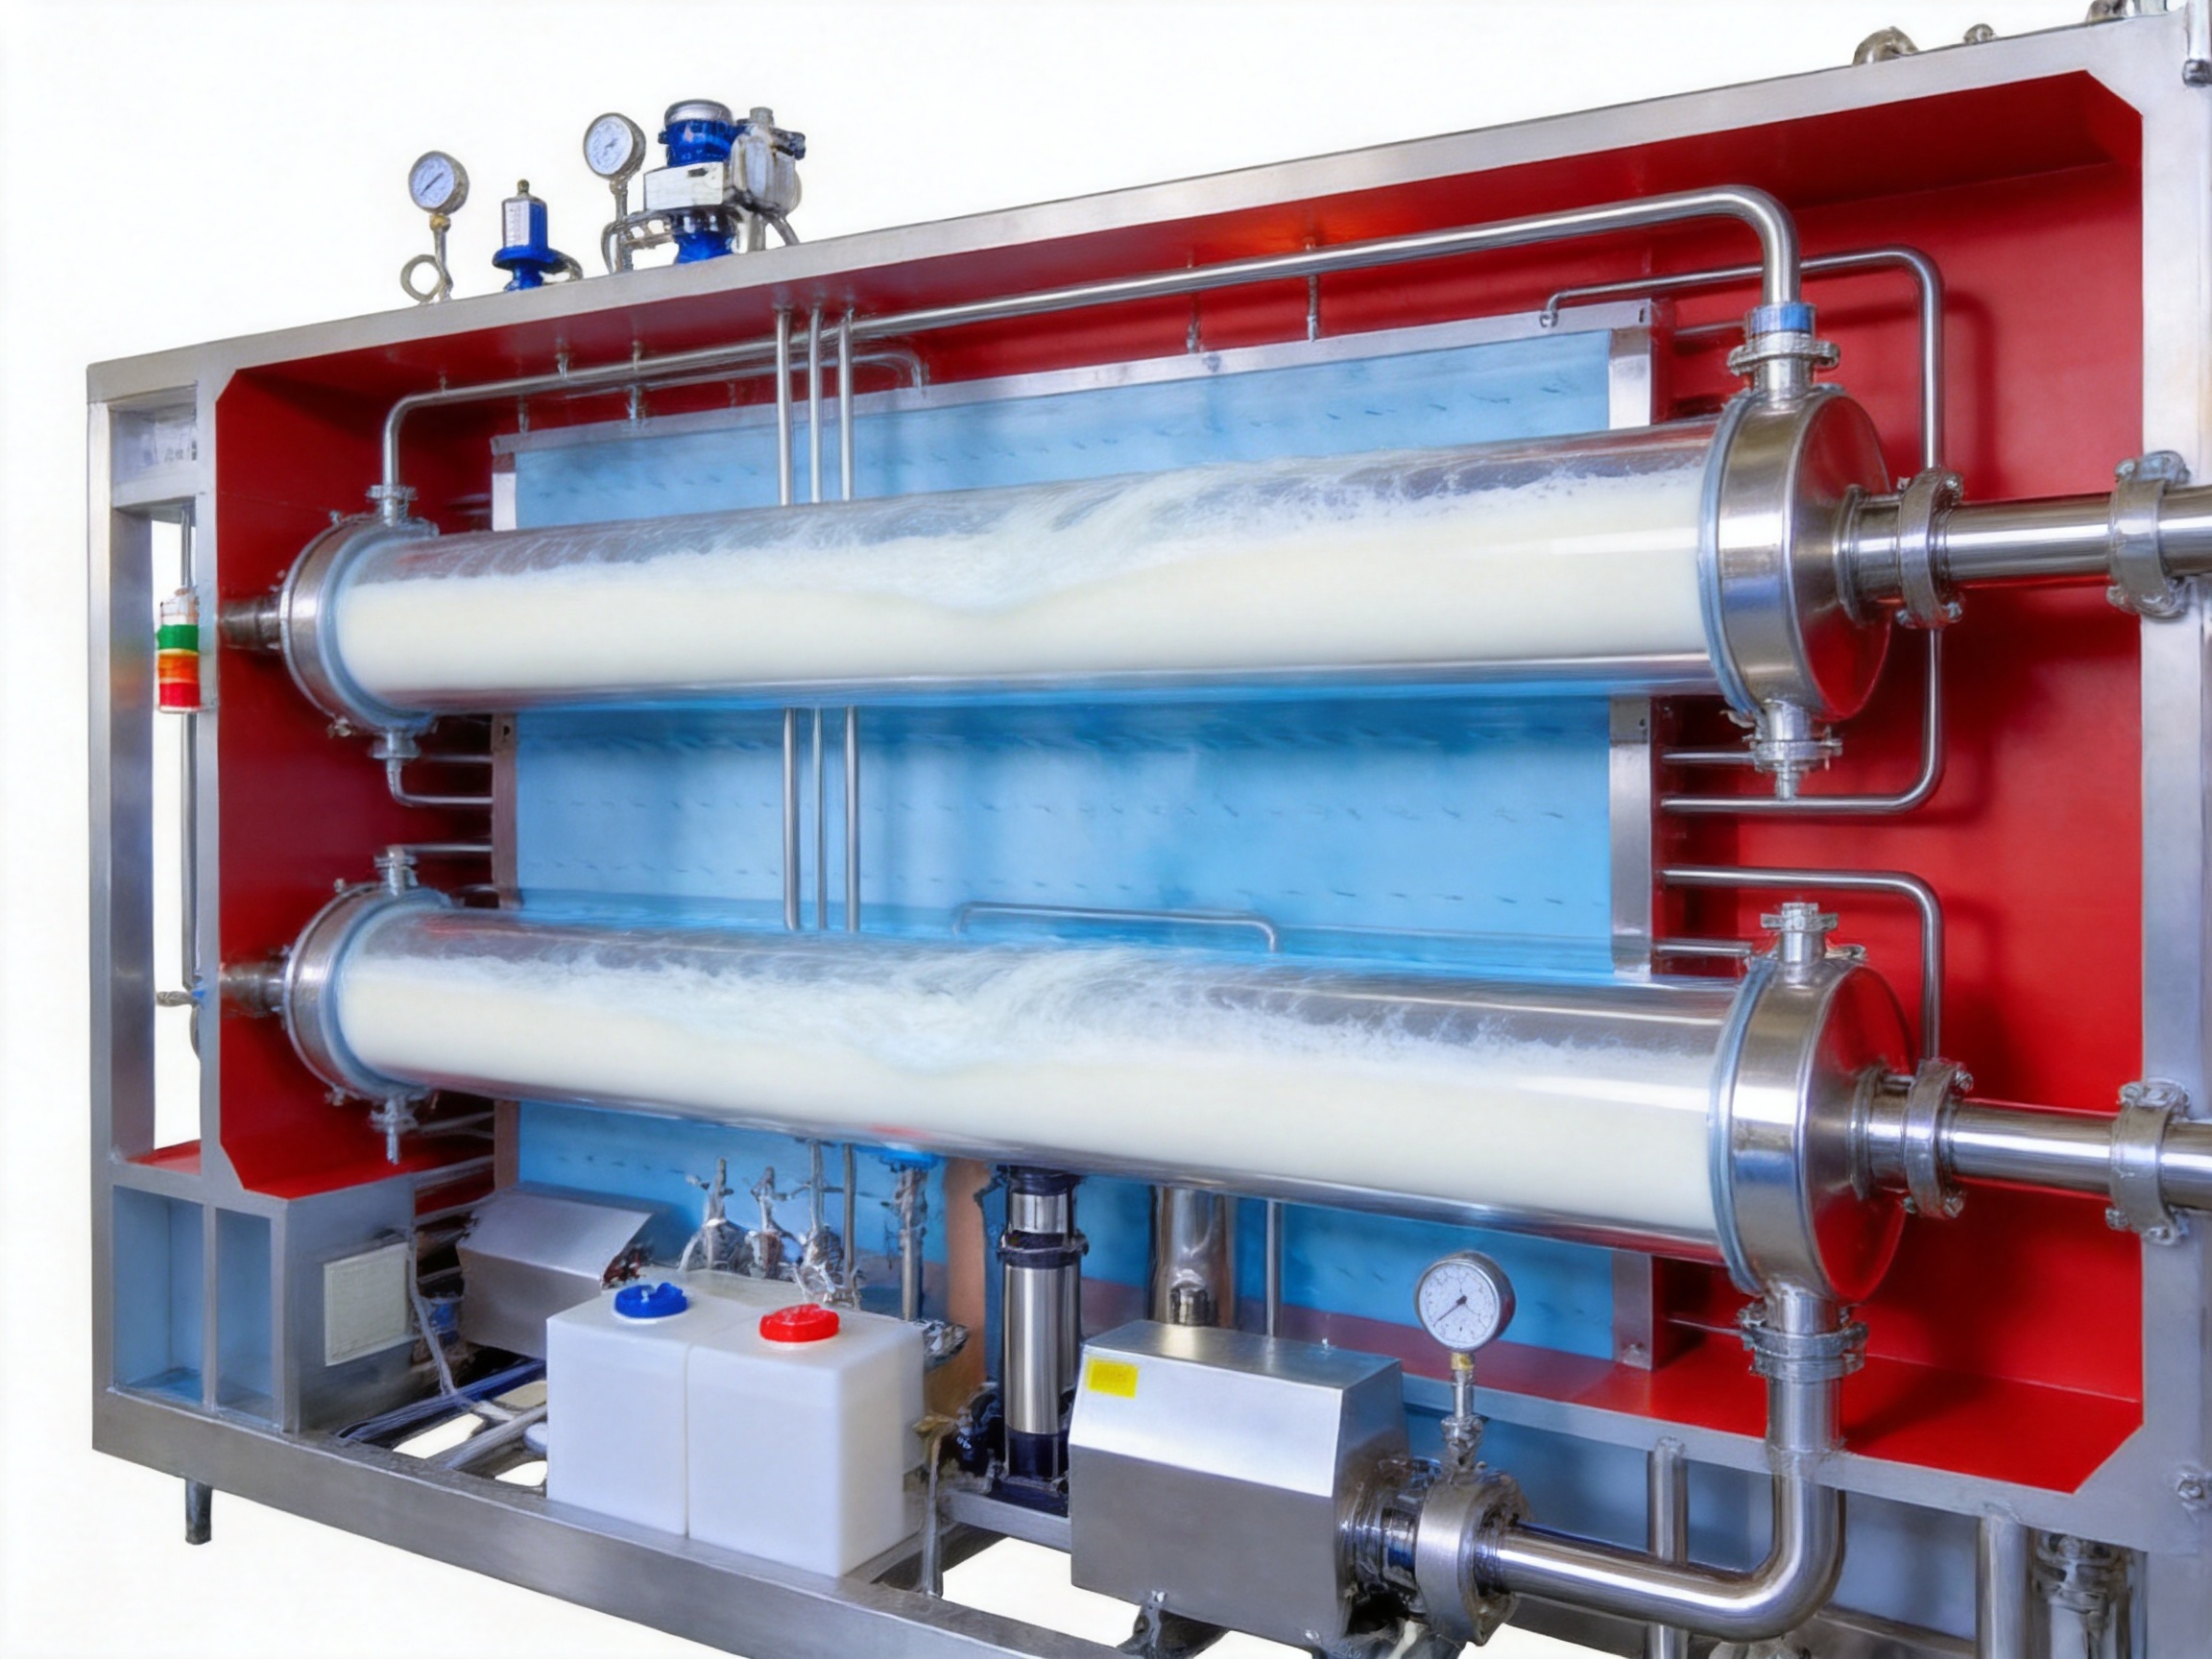
11. Installation, Operation, and Maintenance
11.1 Installation Planning
Installation planning should begin before the equipment arrives at the factory. The customer should confirm the available floor area, access route, lifting capacity, utility connections, drainage, ventilation, control-system interfaces, and maintenance clearance. Skid dimensions and connection locations should be reviewed against the plant layout.
Utility requirements may include electrical power, process water, chilled water, steam, compressed air, cleaning chemicals, and drainage. The actual requirements depend on the system configuration and production capacity. Insufficient utility capacity can prevent the equipment from reaching stable operating conditions, while oversized utilities may increase installation cost.
11.2 Start-Up and Operator Training
Commissioning normally includes mechanical inspection, electrical checks, instrument verification, utility testing, water runs, cleaning-cycle testing, and product trials. Operators should receive training on start-up, shutdown, alarms, product changeover, cleaning, sampling, emergency procedures, and routine inspection.
Clear operating instructions reduce the risk of errors and support consistent production. Training should explain not only which buttons to press, but also why certain conditions are important. Operators who understand the relationship between temperature, flow, pressure, holding time, and product quality are better prepared to respond to deviations.
11.3 Preventive Maintenance
Preventive maintenance may include checking pumps, seals, valves, instruments, control cabinets, insulation, safety devices, and heat-transfer surfaces. Calibration schedules should be established for critical sensors and meters. Gaskets and elastomers should be replaced before failure causes leakage or contamination.
Maintenance records can help identify changes in performance. Increasing pressure drop, longer heating times, unusual pump noise, unstable temperature control, or reduced cleaning effectiveness may indicate fouling, wear, blockage, or instrument drift. Early detection can reduce unplanned downtime.
11.4 Cleaning and Changeover
Cleaning procedures should be based on the actual product residue and validated for the installed equipment. Flow velocity, chemical concentration, temperature, and cleaning time all influence results. The cleaning system should provide adequate circulation through the heat exchanger, holding tube, valves, pumps, and connected piping.
When multiple products are processed on the same line, the changeover sequence should consider allergens, color, flavor, fat, protein, and microbial risk. A well-planned process can reduce water and chemical consumption while maintaining hygiene. The equipment’s drainability and accessible design support faster and more reliable changeovers.
12. Selecting the Right UHT Tube Pasteurizer
Equipment selection should be based on documented process requirements rather than a general capacity estimate. The customer should provide product composition, viscosity range, particle size, target flow rate, inlet temperature, treatment objective, cooling requirement, product-contact material expectations, cleaning procedure, and packaging connection details.
The supplier should then evaluate heat-transfer area, tube dimensions, pump capacity, holding-tube design, utility consumption, control architecture, skid layout, and future expansion. If the product changes significantly during development, the design may need to be reviewed again. This is especially important for new plant-based products, high-protein formulations, sauces, and products with suspended particles.
Customers should also review the supplier’s manufacturing capability. Important questions include whether the supplier controls welding and polishing, how materials are traced, how instruments are calibrated, whether factory testing is available, how documentation is delivered, and what technical support is offered after installation.
Another important consideration is lifecycle value. The lowest purchase price may not represent the lowest total cost if the equipment consumes excessive energy, requires frequent manual cleaning, causes long changeovers, or is difficult to maintain. A well-designed system can provide value through stable production, lower waste, efficient utilities, reliable cleaning, and easier service access.
| Selection Criterion | Questions to Review | Why It Matters |
|---|---|---|
| Product characteristics | What are the viscosity, particle size, solids content, and thermal sensitivities? | Determines tube geometry, pump selection, heat-transfer design, and process limits. |
| Capacity | What is the required hourly flow rate and future expansion target? | Influences heating area, holding volume, utility demand, and skid size. |
| Thermal objective | What temperature, holding time, and cooling conditions are required? | Defines the treatment sections and control strategy. |
| Hygiene | What surface finish, materials, valves, seals, and cleaning standards are required? | Supports product safety, cleanability, and regulatory expectations. |
| Automation | What alarms, recipes, reports, interlocks, and plant interfaces are needed? | Improves repeatability, traceability, and operator control. |
| Utilities | Are steam, water, cooling, electricity, and compressed air available? | Ensures stable operation and accurate project costing. |
| Documentation | What certificates, test records, manuals, and validation support are required? | Supports quality management, commissioning, and future maintenance. |
| Service | What installation, training, spare parts, and after-sales support are available? | Reduces start-up risk and protects long-term equipment performance. |
13. Why Choose a Process-Focused Equipment Partner
A UHT pasteurizer is a process system, not simply a fabricated heat exchanger. Its success depends on the interaction between thermal design, fluid dynamics, hygienic construction, automation, cleaning, utilities, and downstream packaging. A process-focused partner can evaluate these factors together.
Shiloc (Shanghai) Industrial Trading Co., Ltd. provides equipment and engineering support for food and beverage, biopharmaceutical, daily chemical, and fine chemical industries. The company’s capabilities include heat exchangers, aseptic mixing equipment, equipment manufacturing, import and export services, and engineering and technical services.
Its Shanghai operation combines international design concepts with local technical execution. A 3,000-square-meter facility, more than 20 technical specialists, and in-house capabilities for processing, welding, polishing, and quality control provide a foundation for customized equipment projects.
The company emphasizes innovative design, process optimization, safe and efficient equipment, reliable supply, traceability, and personalized customer service. These priorities are relevant to UHT projects because customers often need more than a standard catalogue product. They may require a process review, equipment adaptation, documentation package, installation coordination, and long-term technical support.
The company’s stated values include integrity, pragmatism, innovation, development, excellent quality, and global sharing. In practical terms, these values should be reflected in clear project communication, realistic technical proposals, careful manufacturing, transparent documentation, and responsive service throughout the equipment lifecycle.
14. Sustainability and Long-Term Operating Value
Manufacturers are increasingly evaluating equipment according to energy, water, waste, and maintenance performance. A UHT system can contribute to sustainability when it uses regenerative heat recovery, efficient pumps, insulated hot surfaces, optimized cleaning cycles, and accurate controls.
Reducing product waste is another important benefit. Stable start-up, reliable product diversion, accurate temperature control, and efficient changeover can reduce the quantity of product sent to drain. Improved cleaning design can also reduce water and chemical consumption, provided that the cleaning cycle is validated and properly controlled.
Long-term value depends on reliability. Equipment that is easy to inspect, clean, repair, and upgrade is more likely to remain productive over many years. Modular control systems, accessible instruments, replaceable wear components, and clear documentation can make future maintenance more efficient.
Sustainability should be considered during the design stage rather than treated as an afterthought. The supplier and customer can review heat recovery, utility sizing, production scheduling, cleaning procedures, and equipment layout together. Small design improvements can produce meaningful savings over the life of the system.
15. Future Development of Tube-Based UHT Systems
Future UHT systems are likely to place greater emphasis on digital monitoring, energy optimization, predictive maintenance, and flexible production. More detailed process data can help manufacturers identify fouling trends, compare batches, monitor utility performance, and improve cleaning schedules.
Automation may also support more precise recipe management and product changeover. Digital records can provide stronger traceability and help quality teams investigate deviations. However, digital tools are most effective when the underlying mechanical system is correctly designed and the instruments provide trustworthy measurements.
Product innovation will continue to influence equipment design. The growth of plant-based beverages, high-protein drinks, functional nutrition, specialty sauces, and complex emulsions creates demand for systems that can handle broader viscosity ranges and more challenging formulations.
Equipment manufacturers with combined design, fabrication, process engineering, and service capabilities will be well positioned to support this development. The ability to adapt tube geometry, heat recovery, automation, surface finish, cleaning strategy, and integration details will remain a major competitive advantage.
16. Frequently Asked Questions
What is an Ultra-High Temperature Tube Pasteurizer?
An Ultra-High Temperature Tube Pasteurizer is a continuous thermal processing system that heats liquid products through sanitary tubes, holds them at a controlled treatment condition for a defined period, and then cools them before further processing or filling. The system can include heating, regeneration, holding, cooling, pumping, instrumentation, valves, and automated controls.
How is a tubular system different from a plate heat exchanger?
A tubular system transfers heat through tubes and can often provide a more robust flow path for products containing particles, fibers, or higher viscosity. A plate heat exchanger uses narrow channels between plates and can be highly efficient for compatible low-viscosity liquids. The best option depends on product composition, fouling behavior, capacity, cleaning requirements, and process conditions.
Can the pasteurizer process products with particles?
It can be designed for selected particulate products, provided that the particle size, concentration, shape, and product viscosity are suitable. Tube diameter, pump type, valve design, flow velocity, and pressure drop must be evaluated during engineering. The customer should provide complete product data before the system is designed.
Does the system reduce energy consumption?
It can reduce energy consumption through regenerative heat exchange, insulation, efficient pumps, optimized utility control, and appropriate heating and cooling design. Actual savings depend on the product, capacity, temperature profile, operating schedule, and utility conditions.
Is the system suitable for biopharmaceutical manufacturing?
It may be suitable for selected heat-compatible liquids, buffers, media components, or support process streams. Many biological products are heat-sensitive and cannot undergo UHT treatment. Each application must be reviewed by the customer’s process and quality teams, with suitable qualification and validation requirements established before purchase.
How is hygienic design achieved?
Hygienic design involves suitable product-contact materials, smooth and cleanable surfaces, controlled welds, sanitary valves and fittings, minimized dead legs, proper drainability, compatible seals, and effective clean-in-place circulation. The design should be matched to the product, cleaning chemicals, temperature, and regulatory expectations.
What manufacturing capabilities support the equipment?
Shiloc operates a Shanghai facility with processing, welding, polishing, and quality-control capabilities. The company combines European know-how and Danish design principles with local manufacturing and engineering support. Its technical team supports equipment customization, process optimization, documentation, and project coordination.
Can the pasteurizer be customized?
Yes. Customization may include capacity, tube dimensions, heating and cooling stages, regeneration, holding time, pump configuration, valves, instruments, automation, skid layout, materials, connections, and cleaning interfaces. Customization should be based on documented process requirements to avoid unnecessary complexity.
What information should a customer provide for a quotation?
Useful information includes product type, composition, viscosity, solids and particle content, target capacity, inlet and outlet temperatures, treatment objective, cooling requirement, cleaning method, available utilities, packaging connection, installation location, automation expectations, and documentation requirements.
What support may be required after delivery?
Support may include installation assistance, commissioning, factory acceptance testing, operator training, process trials, documentation, spare parts, calibration guidance, cleaning verification, and troubleshooting. The scope should be agreed during the project planning stage.
Conclusion
The Ultra-High Temperature Tube Pasteurizer provides manufacturers with a flexible and hygienic platform for continuous thermal processing. Its principal strengths include controlled heating and holding, suitability for a broad range of liquid products, compatibility with selected particulate and viscous formulations, regenerative energy recovery, clean-in-place capability, and integration with automated production lines.
Its advantages over competing technologies depend on the application, but tubular construction can offer a particularly strong balance of product flexibility, robust flow handling, hygienic design, and scalable production. When correctly engineered, the system can help manufacturers improve consistency, reduce waste, manage utilities, and support reliable downstream filling.
The manufacturing partner is equally important. Shiloc (Shanghai) Industrial Trading Co., Ltd. combines European know-how, Danish design principles, Shanghai-based fabrication, controlled welding and polishing, quality control, process engineering, and technical service. Its facility, technical specialists, and experience with food, beverage, biopharmaceutical, daily chemical, and fine chemical applications provide a foundation for customized process equipment.
For companies planning a new thermal processing line or upgrading an existing facility, the most effective approach is to evaluate the complete process. Product properties, thermal requirements, cleaning, automation, utilities, documentation, installation, and lifecycle support should all be considered together. With the right engineering design and manufacturing discipline, a tube-based UHT system can become a reliable, efficient, and adaptable part of a modern production facility.
References
1. Codex Alimentarius Commission. General Principles of Food Hygiene and Hygienic Practice for Milk and Milk Products.
2. International Dairy Federation. Principles of Hygienic Design and Thermal Processing in Dairy Applications.
3. European Hygienic Engineering and Design Group. Hygienic Design Principles for Food Processing Equipment.
4. United States Food and Drug Administration. Current Good Manufacturing Practice, Hazard Analysis, and Risk-Based Preventive Controls for Human Food.
5. International Organization for Standardization. Quality Management Systems and General Requirements for Competence of Testing and Calibration Laboratories.
6. International Society for Pharmaceutical Engineering. Good Practice Guides for Biopharmaceutical Process Equipment and Facility Design.
7. Perry’s Chemical Engineers’ Handbook. Heat Transfer, Fluid Flow, and Process Equipment Design.
8. Walstra, P., Wouters, J. T. M., and Geurts, T. J. Dairy Science and Technology: Principles of Milk Processing and Thermal Treatment.
9. Lewis, M. J., and Heppell, N. J. Continuous Thermal Processing of Foods: Pasteurization and Sterilization Principles.
10. Shiloc (Shanghai) Industrial Trading Co., Ltd. Technical information concerning process systems, heat exchangers, aseptic mixing equipment, hygienic manufacturing, and engineering services.
Product: Ultra-High Temperature Tube Pasteurizer (UHT)
PREV:Wound Tube Heat Exchangers for Efficient, Reliable Industrial Processing
NEXT:Bottom-Mounted Magnetic Mixers for Hygienic Food, Beverage, and Biopharmaceutical Processing
NEXT:Bottom-Mounted Magnetic Mixers for Hygienic Food, Beverage, and Biopharmaceutical Processing
Interested in cooperation or have questions?
Recommended LINS
✦
Food Processing Skid System
Food and Beverage Process System
Aseptic Processing Equipment for Liquid Foods
High Temperature Short Time Sterilizer
CIP Skid System for Food Industry
UHT Processing Equipment for Plant Based Milk
UHT Processing System for Dairy Products
Tubular Pasteurizer for Fruit Puree
CIP process skid system for food industry
automated process skid system for food processing
Let'S Work Together Welcome Aboard!
-

haikexin@haikexin.com
+8613391278930
-
 +86-21-57560276
-
 No. 2819, Sihu Road,Fengxian District, Shanghai, China
Join Our Mailing List
Copyright © Shiloc (Shanghai) Industrial Trading Co., Ltd. All Rights Reserved.
Process Systems & Equipment For Food & Biopharma Manufacturers
